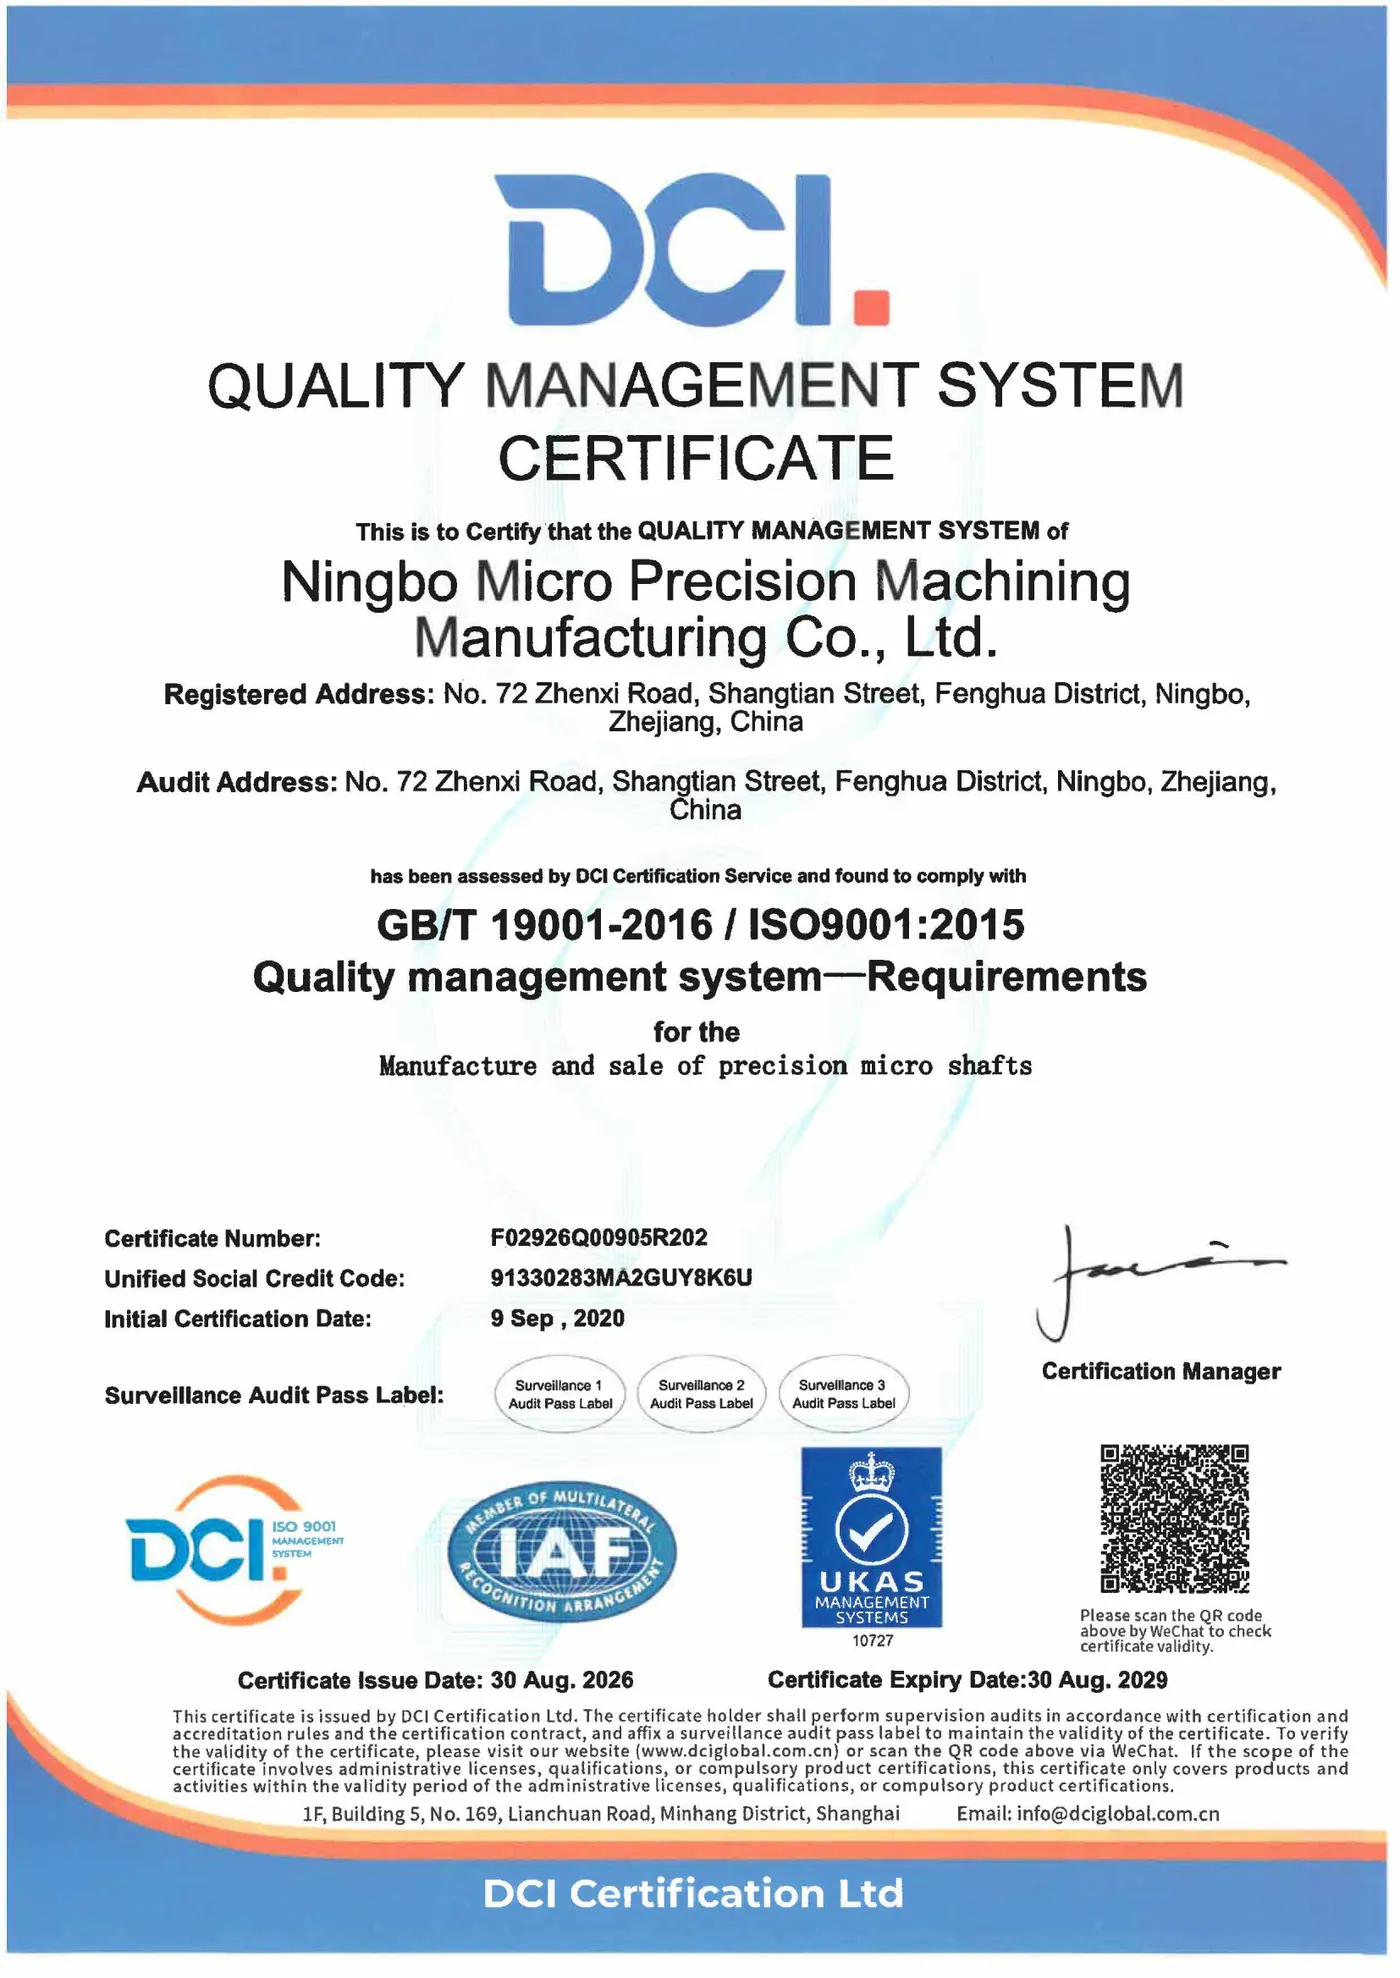
ISO 9001:2015
Quality management system
Production runs under ISO 9001, ISO 14001 and IATF 16949. Parts are checked against your drawing and inspection plan before they ship.
Dimensions, tolerances, appearance, material, hardness, roughness and treatment requirements are checked against the drawing and inspection plan.
Camera sorting covers 100% of the appearance and dimension items defined for the part. Items not defined in the plan are not covered by full inspection.
PPAP documentation and Cpk analysis (using Minitab) are provided by project. List the PPAP level, key characteristics and targets on your inquiry so that engineering and quality can confirm them.
ERP and MES systems hold production and quality records.
If parts do not meet requirements, contact us with the order details. Quality and engineering investigate and agree the next steps with you.
All three certificates are held by Ningbo Micro Precision Machining Manufacturing Co., Ltd. for the Ningbo site at No. 72 Zhenxi Road. Details are taken from the certificates; ask us for current copies.
Quality management system
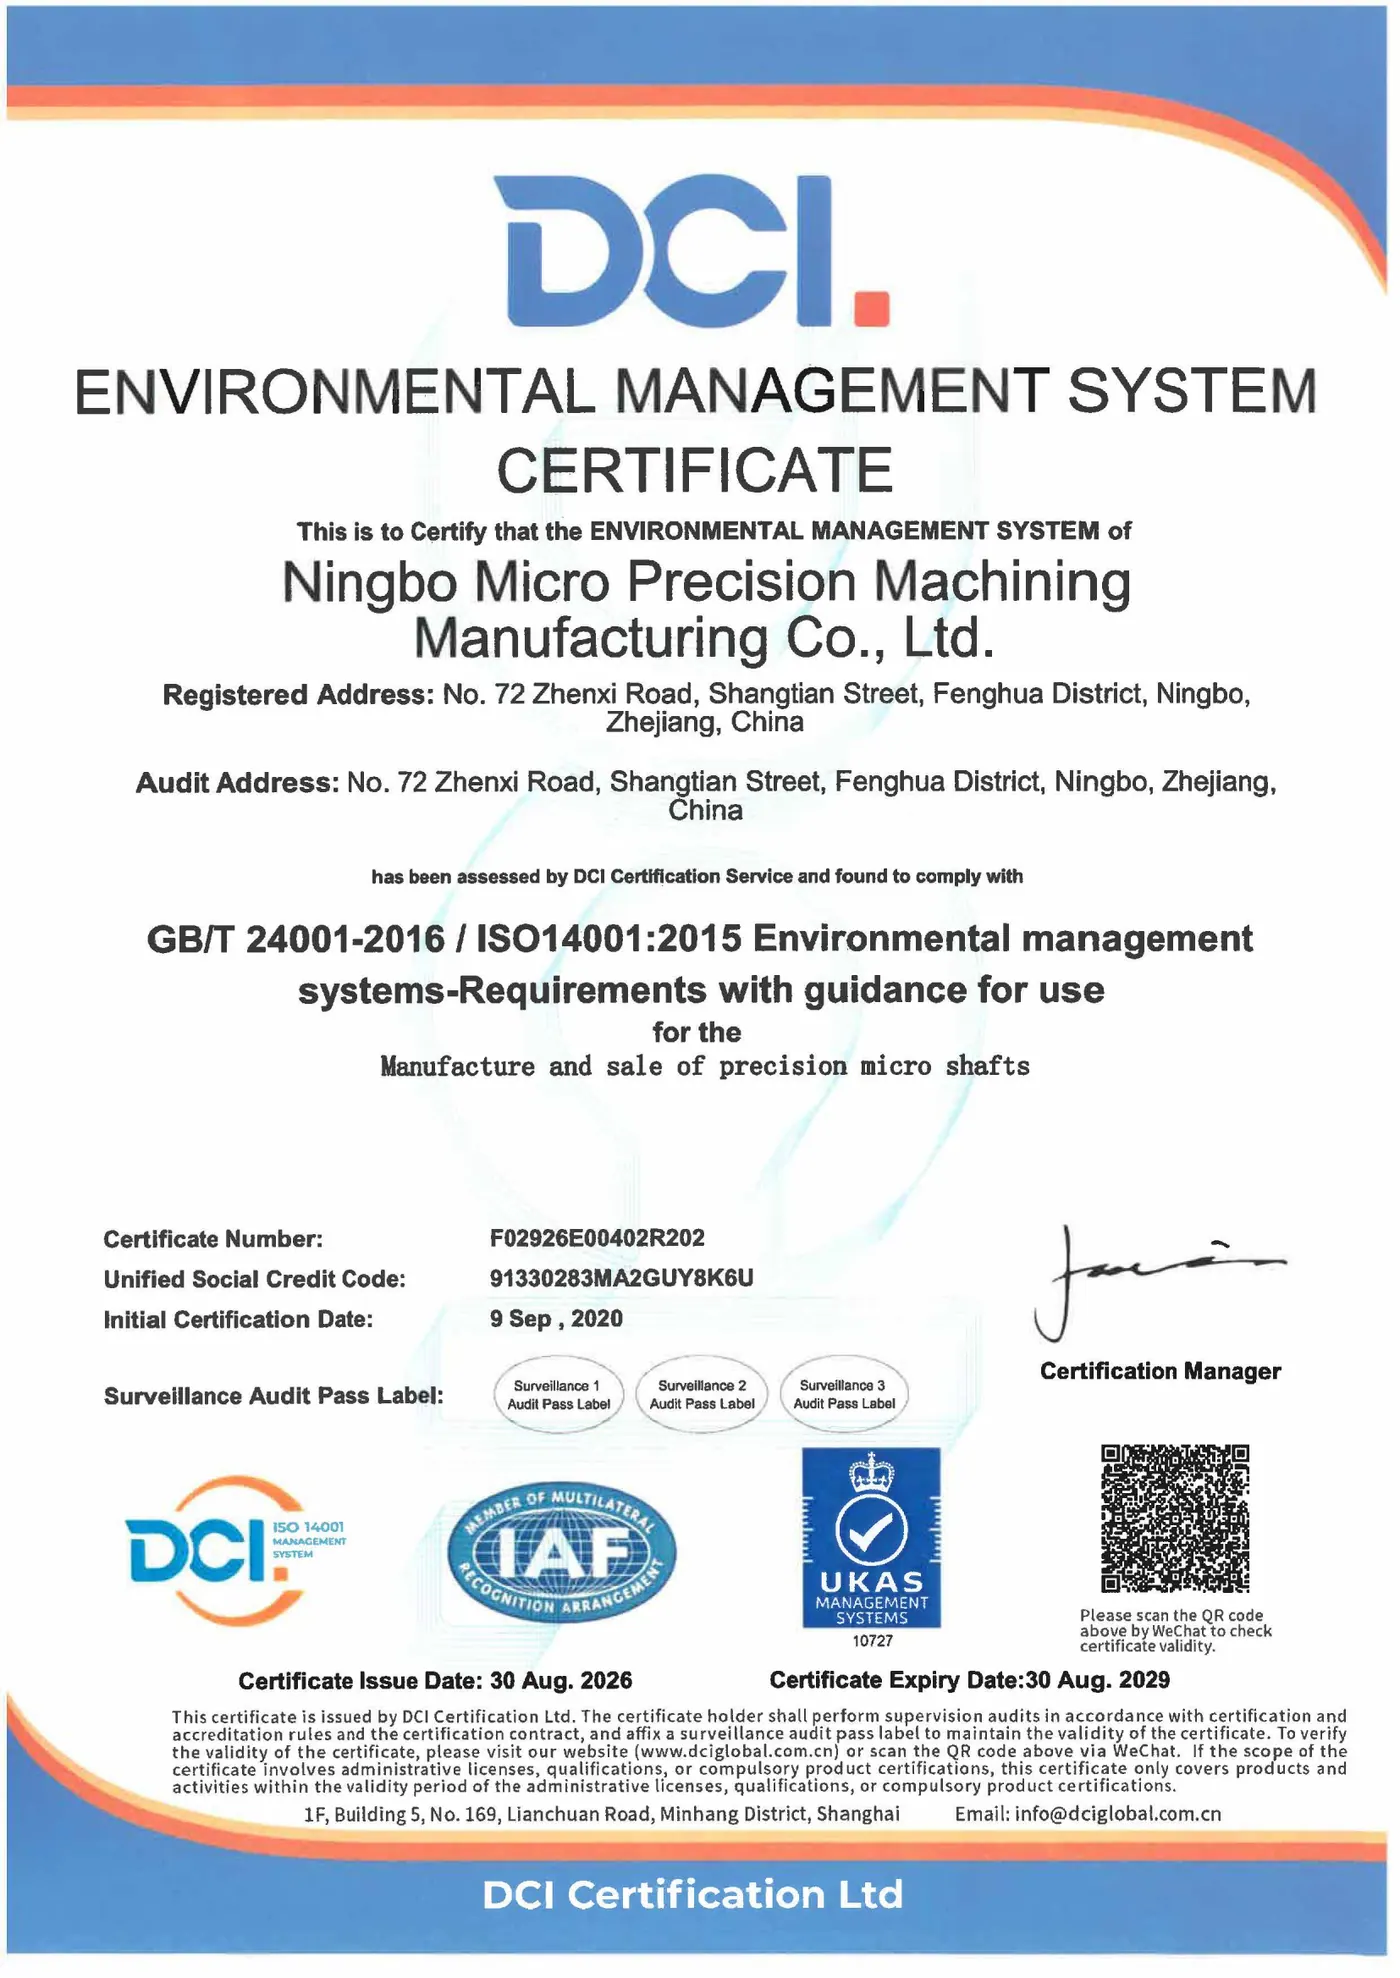
Environmental management system
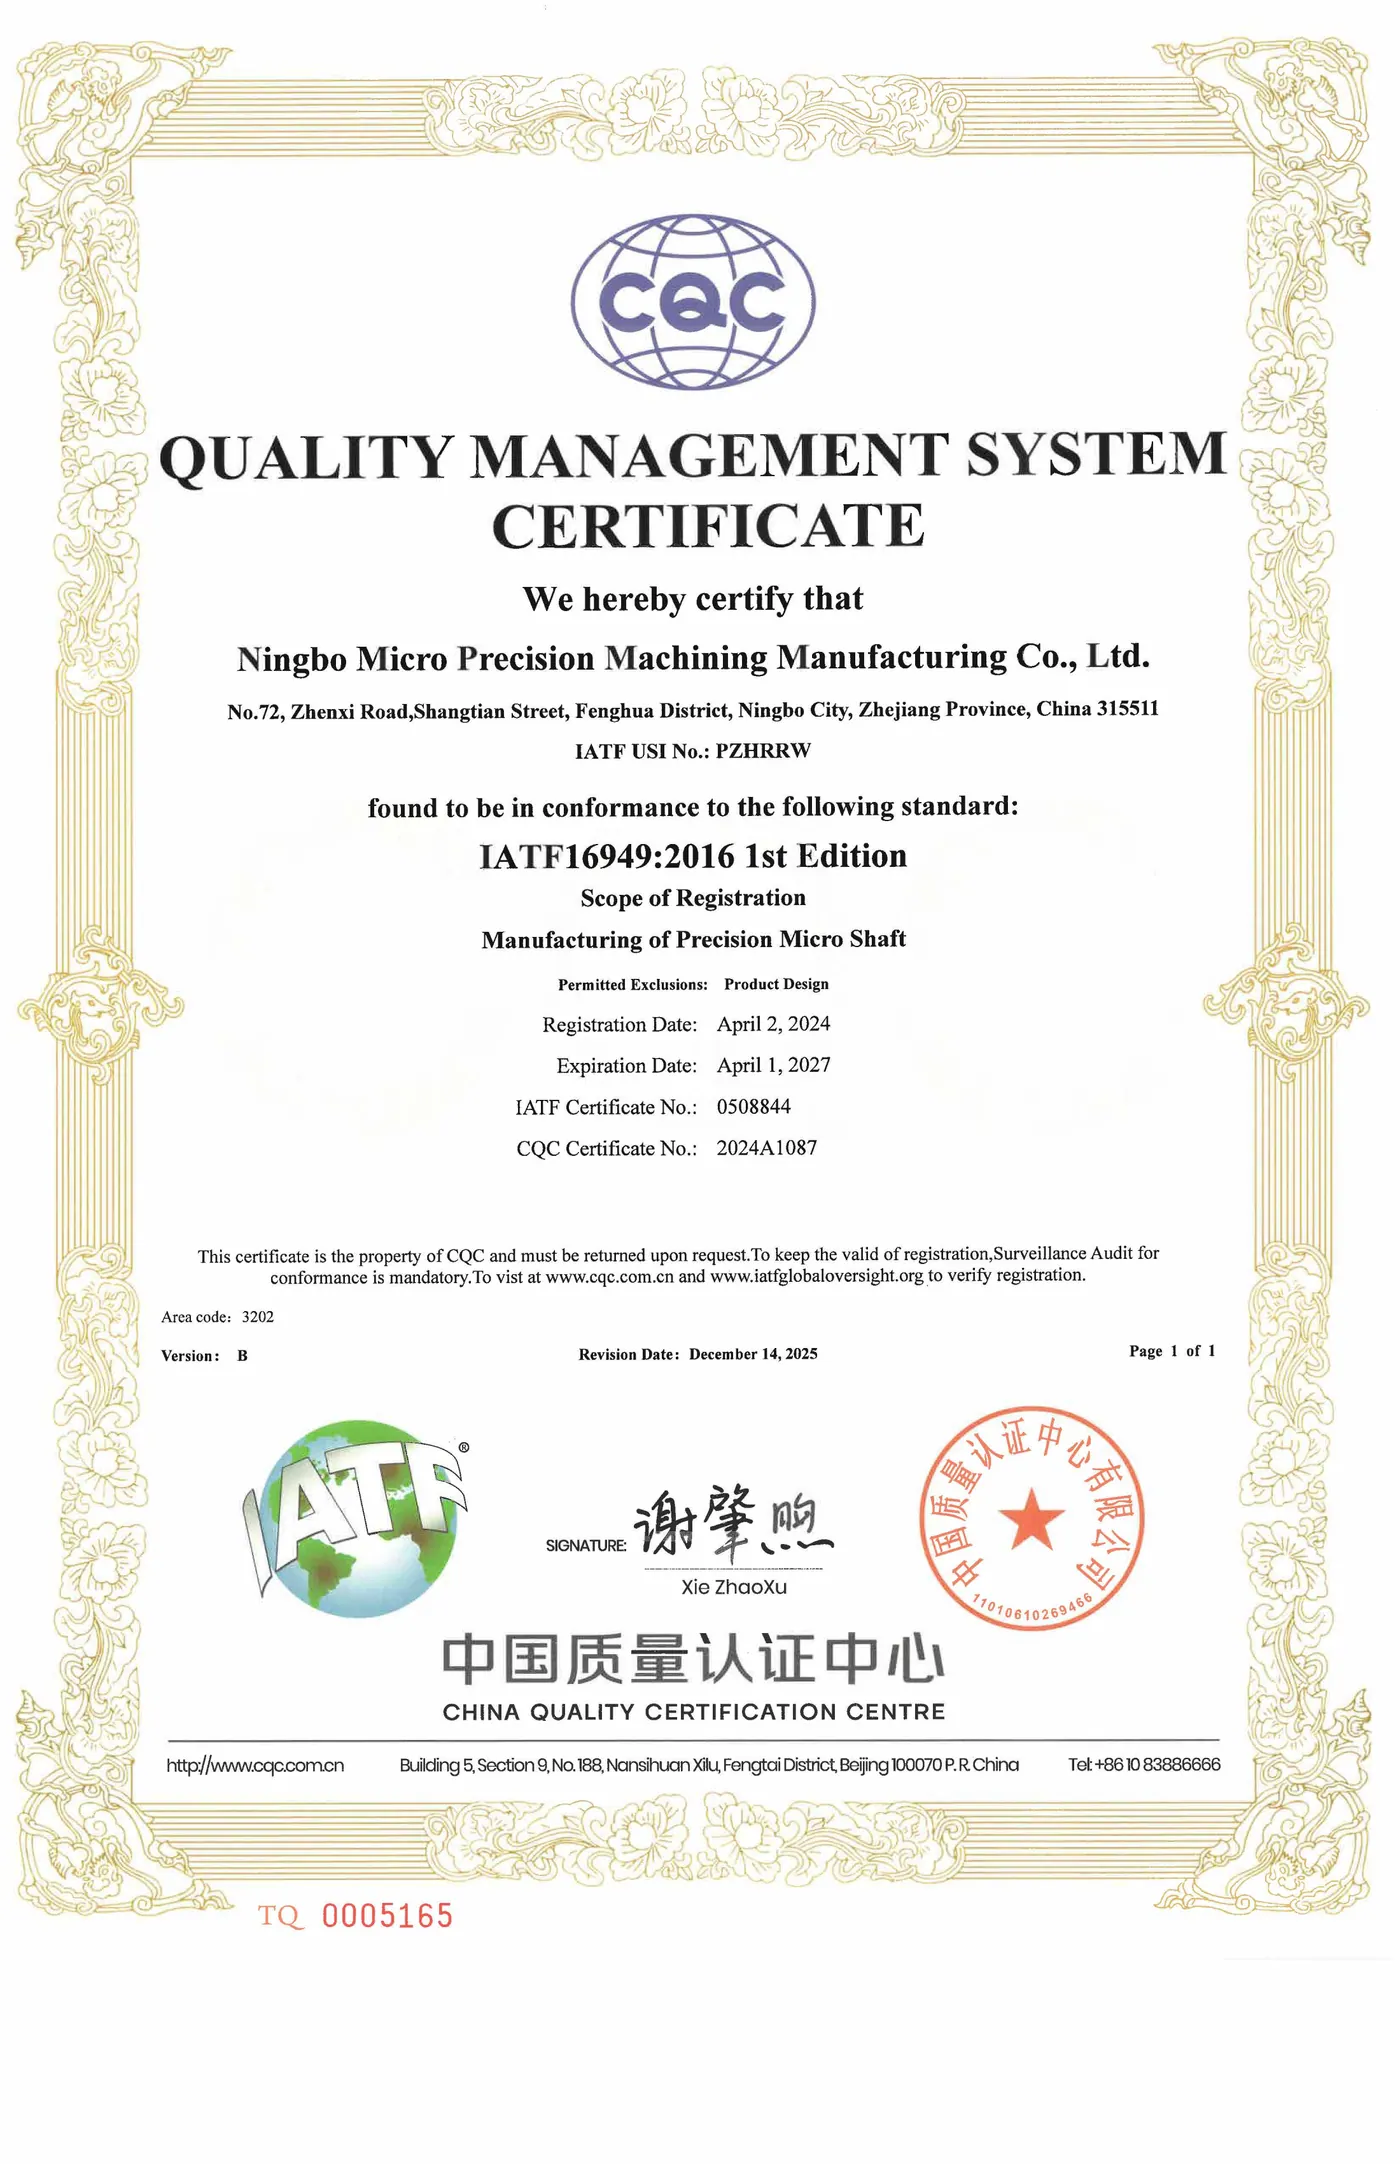
Automotive quality management system
Instruments used for dimensional, material, hardness, roughness and coating checks.
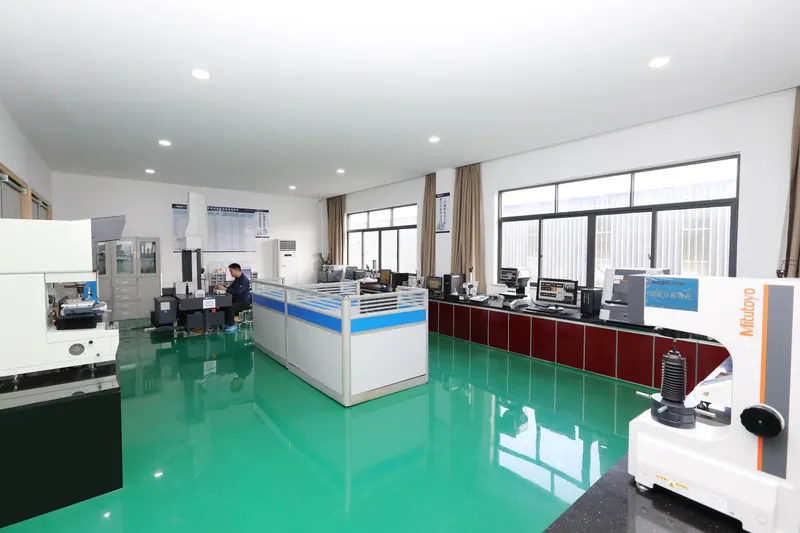
Measurement and inspection resources support checks against the drawing and agreed inspection plan. The method and reporting scope are confirmed for each component.
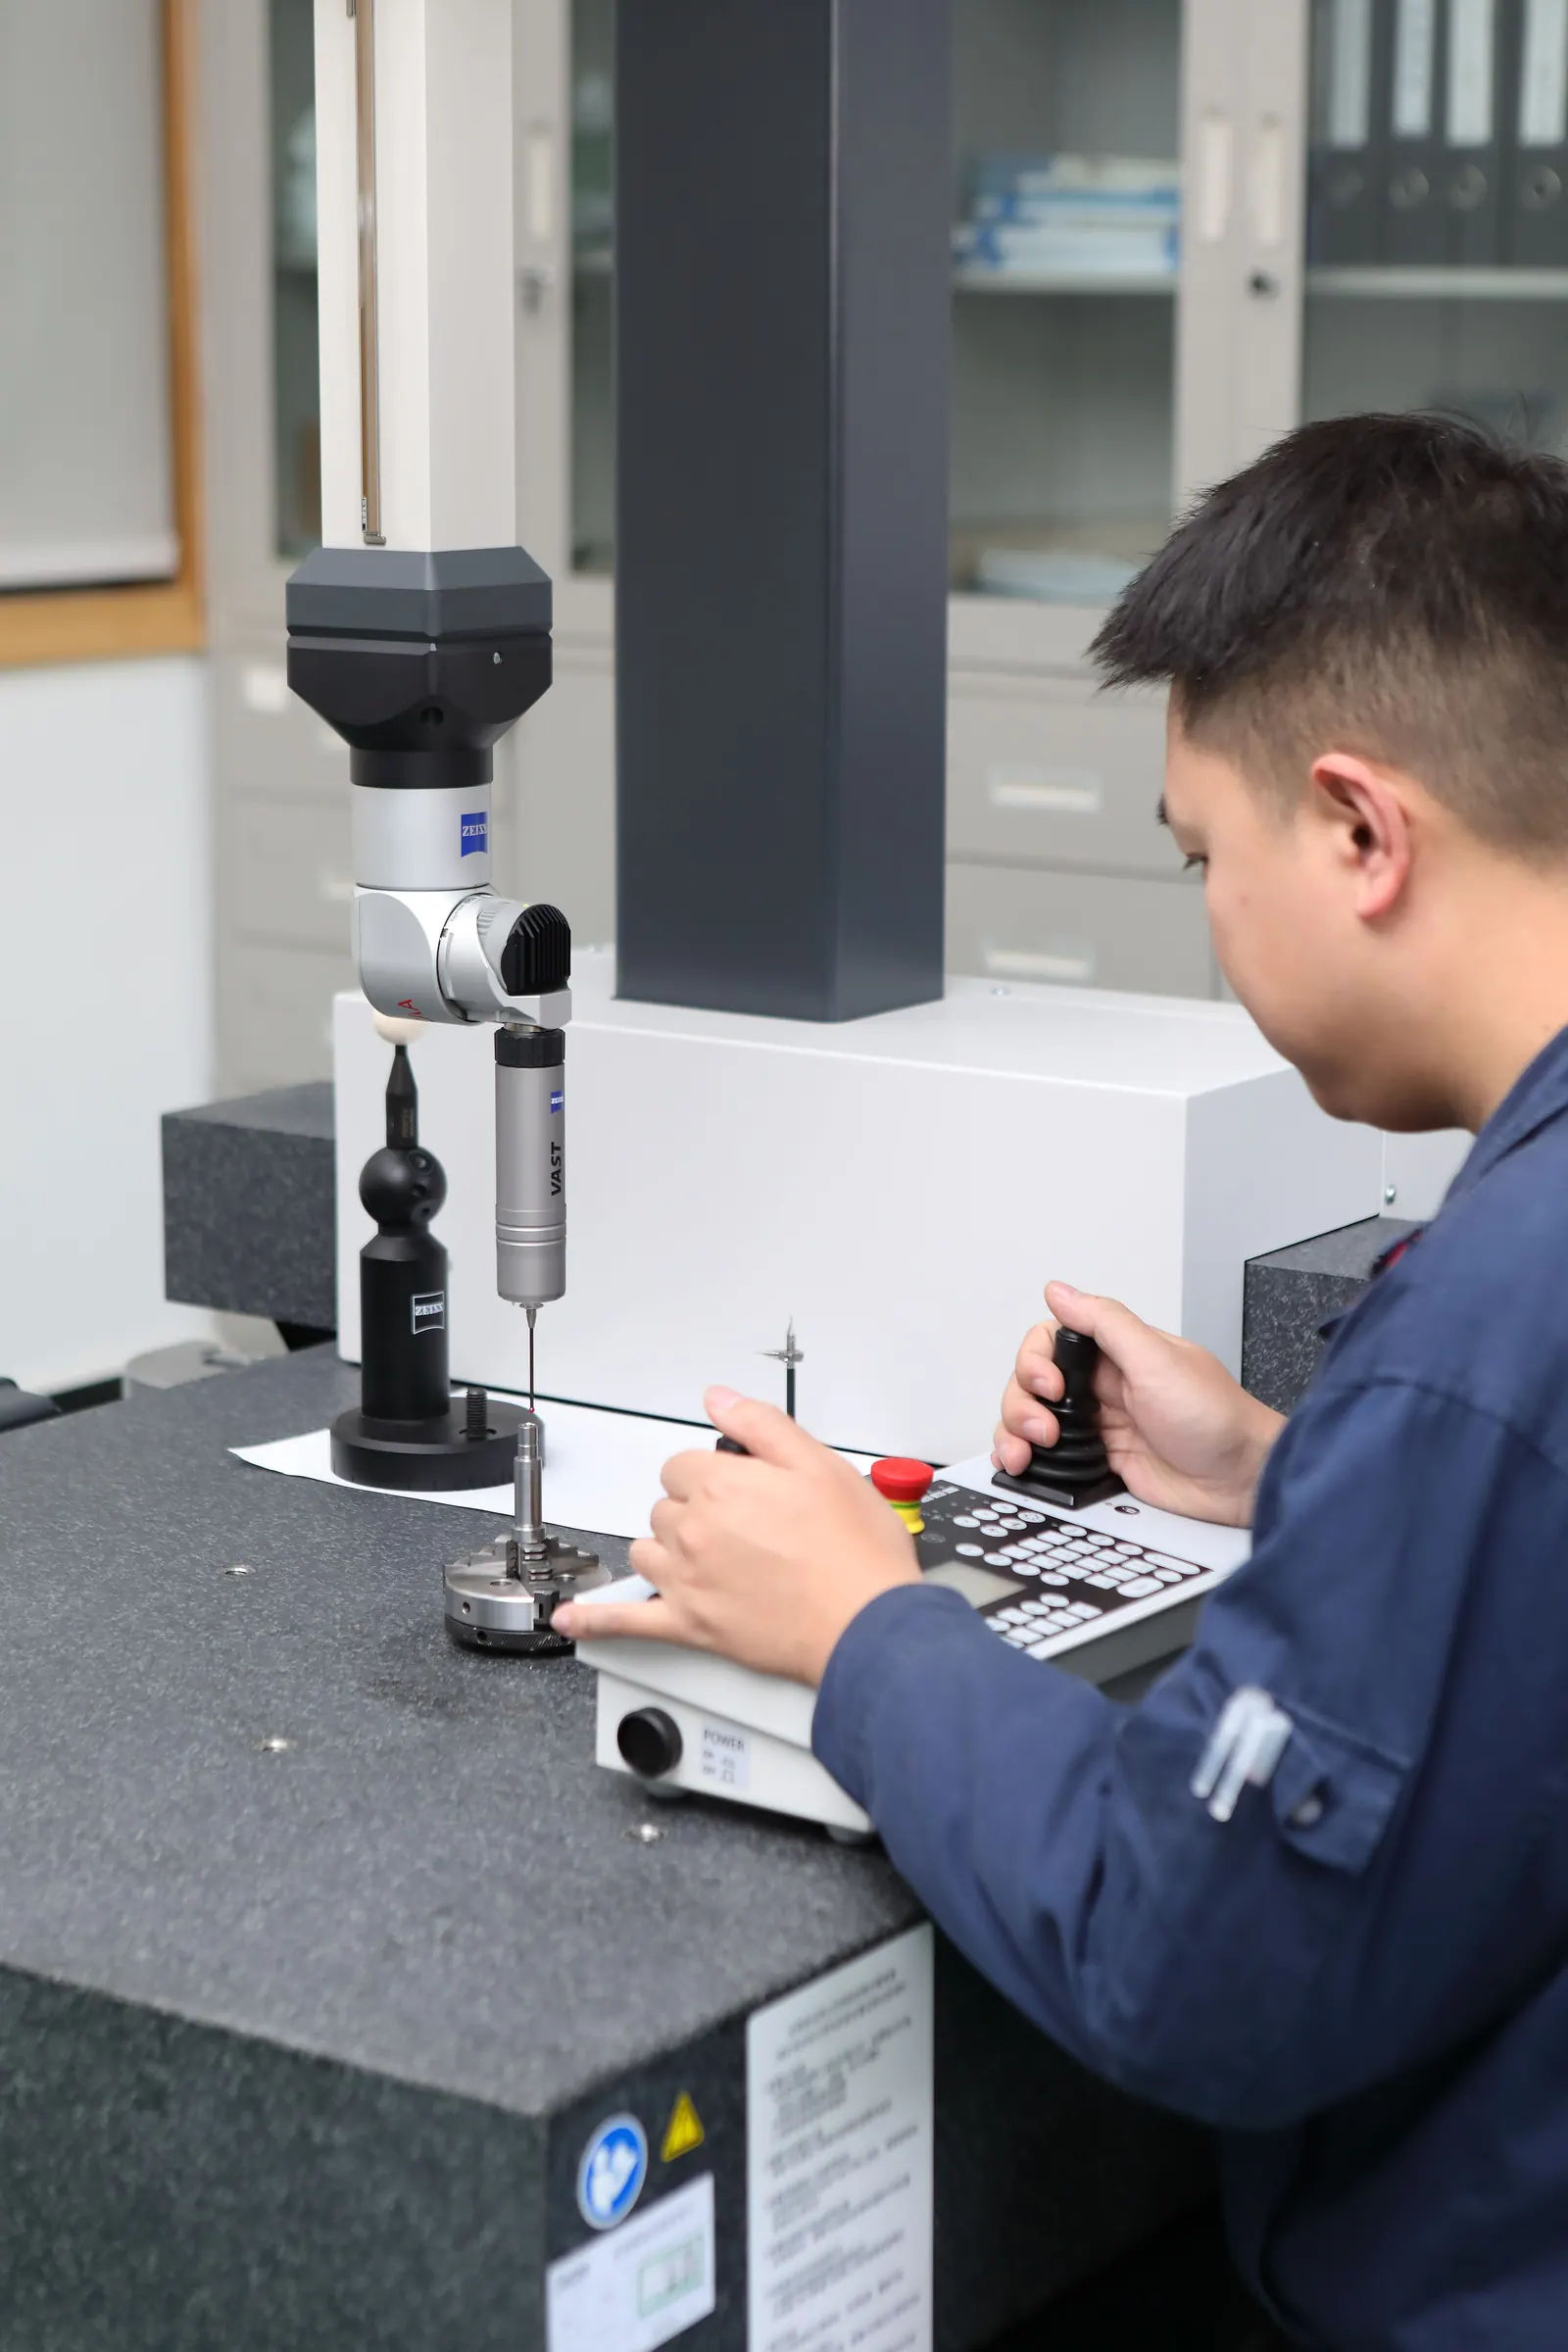
Dimensional and geometric checks against specified drawing characteristics.
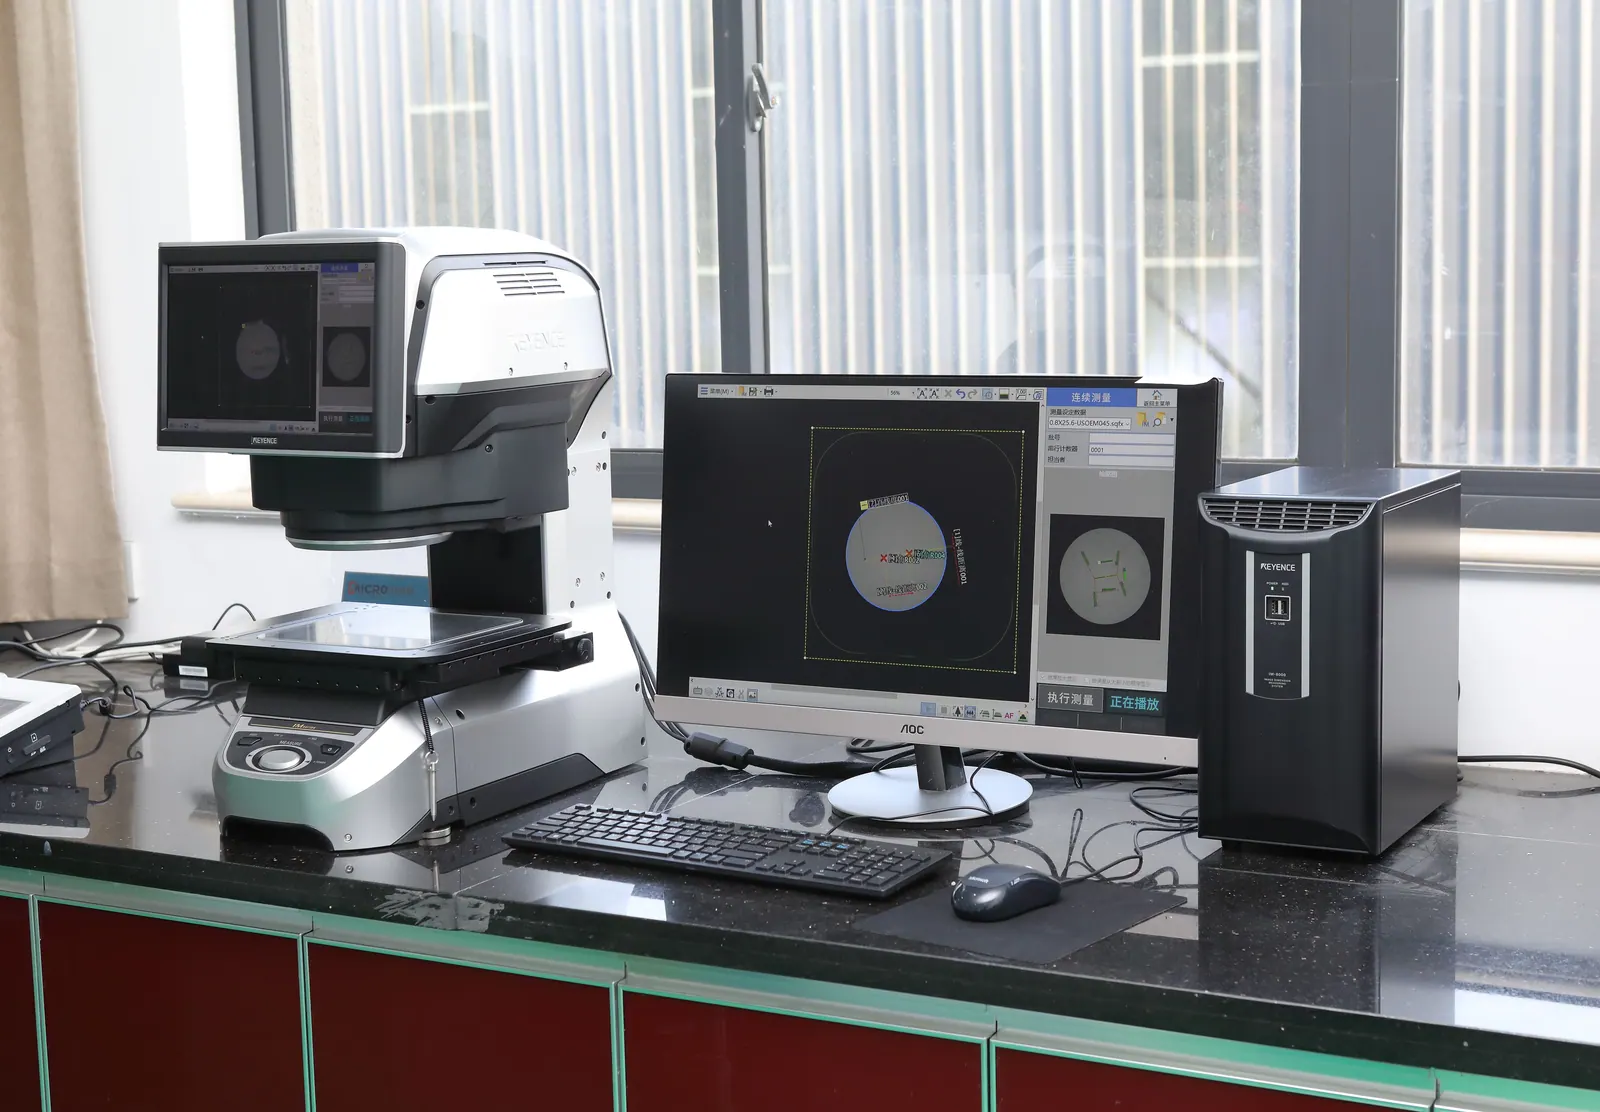
Optical measurement of the dimensions defined in the inspection plan.
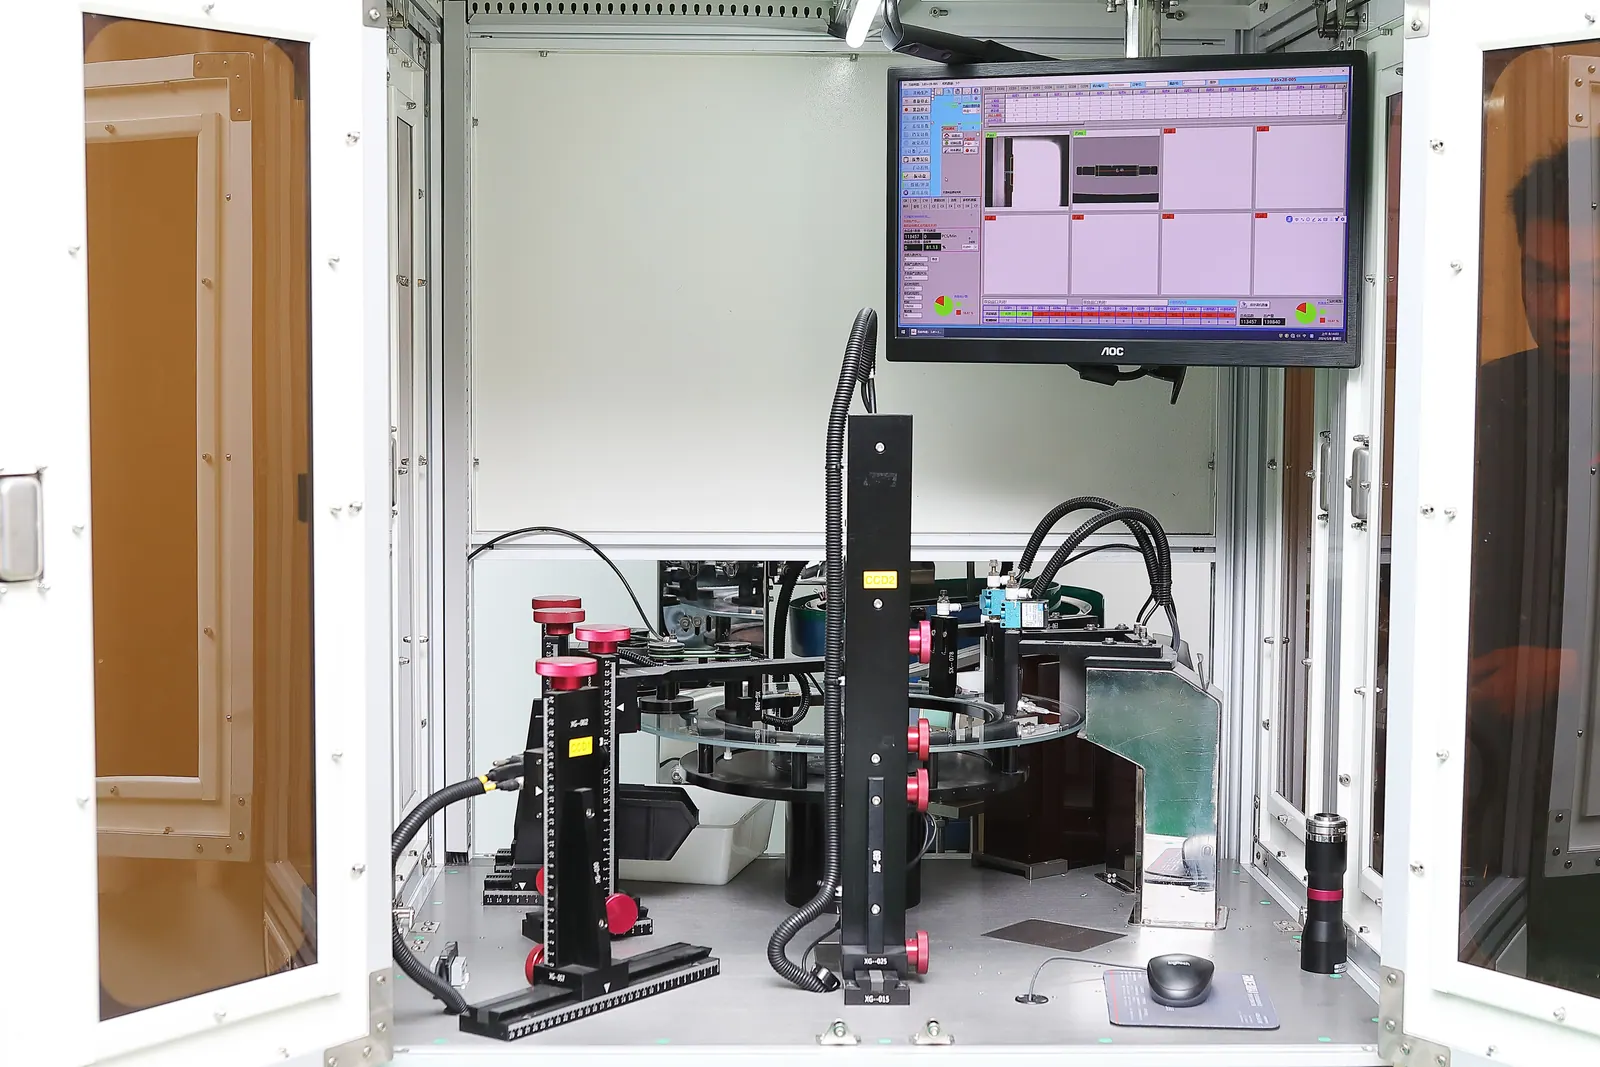
Camera sorting of the appearance and dimensional items defined for the part.
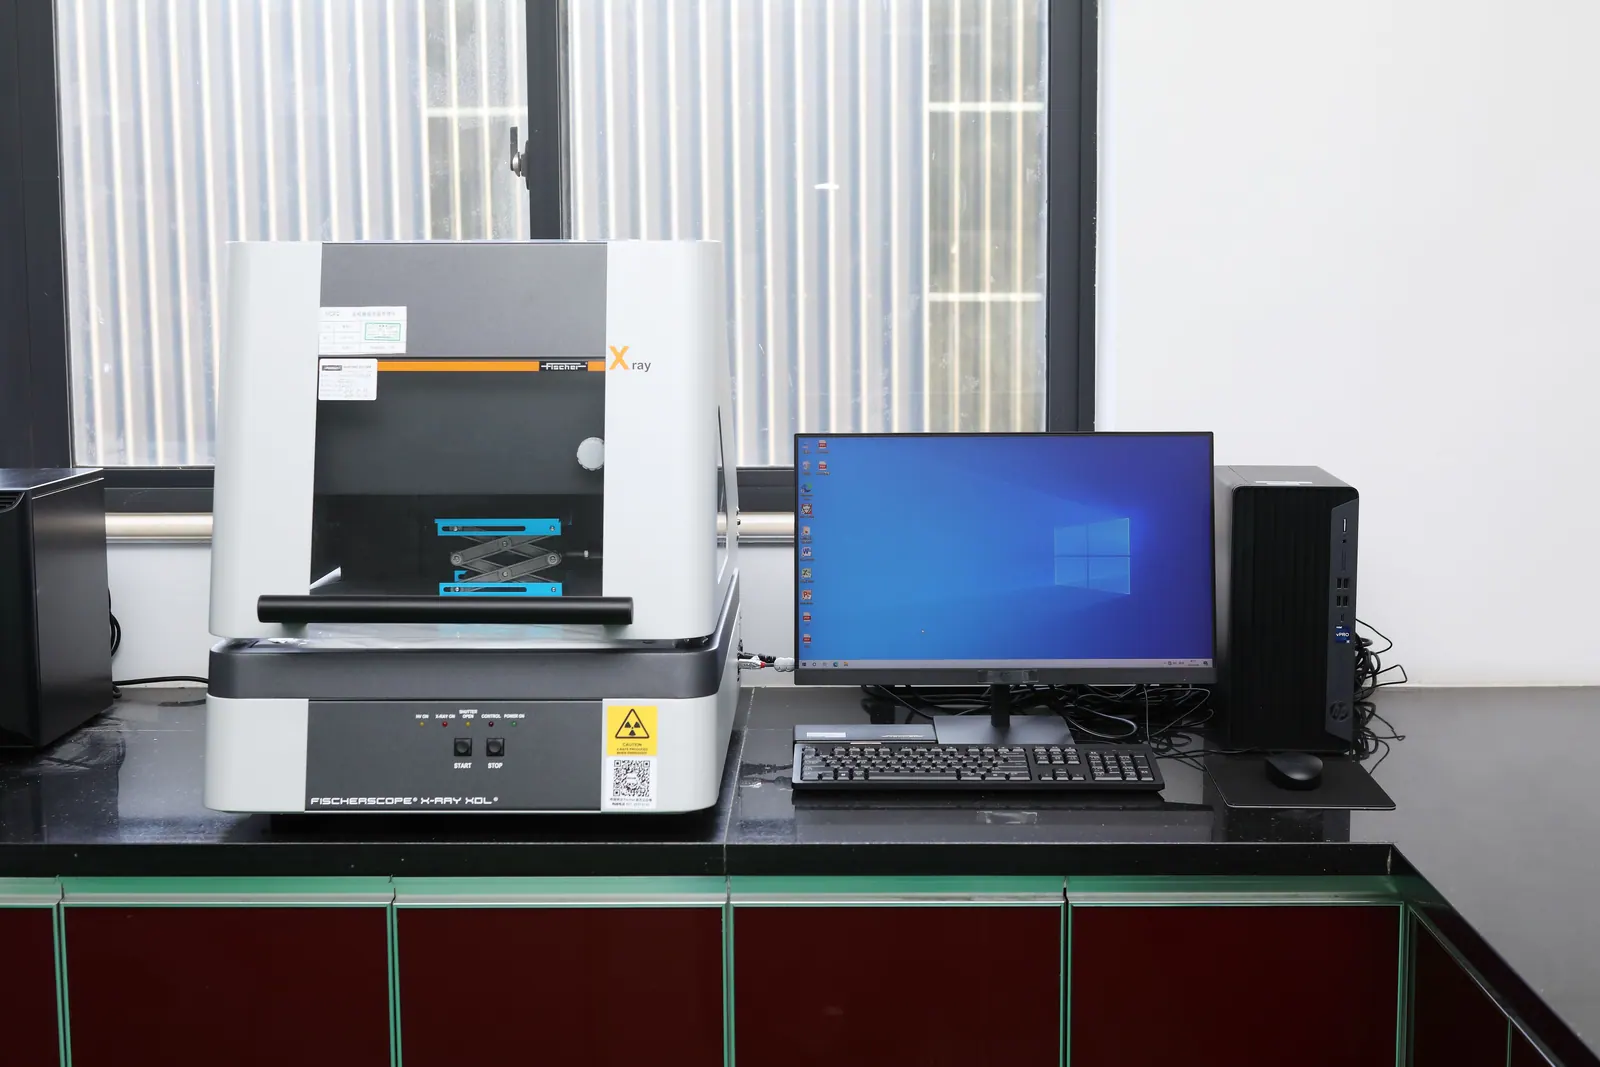
Coating checks according to the specified treatment requirements.
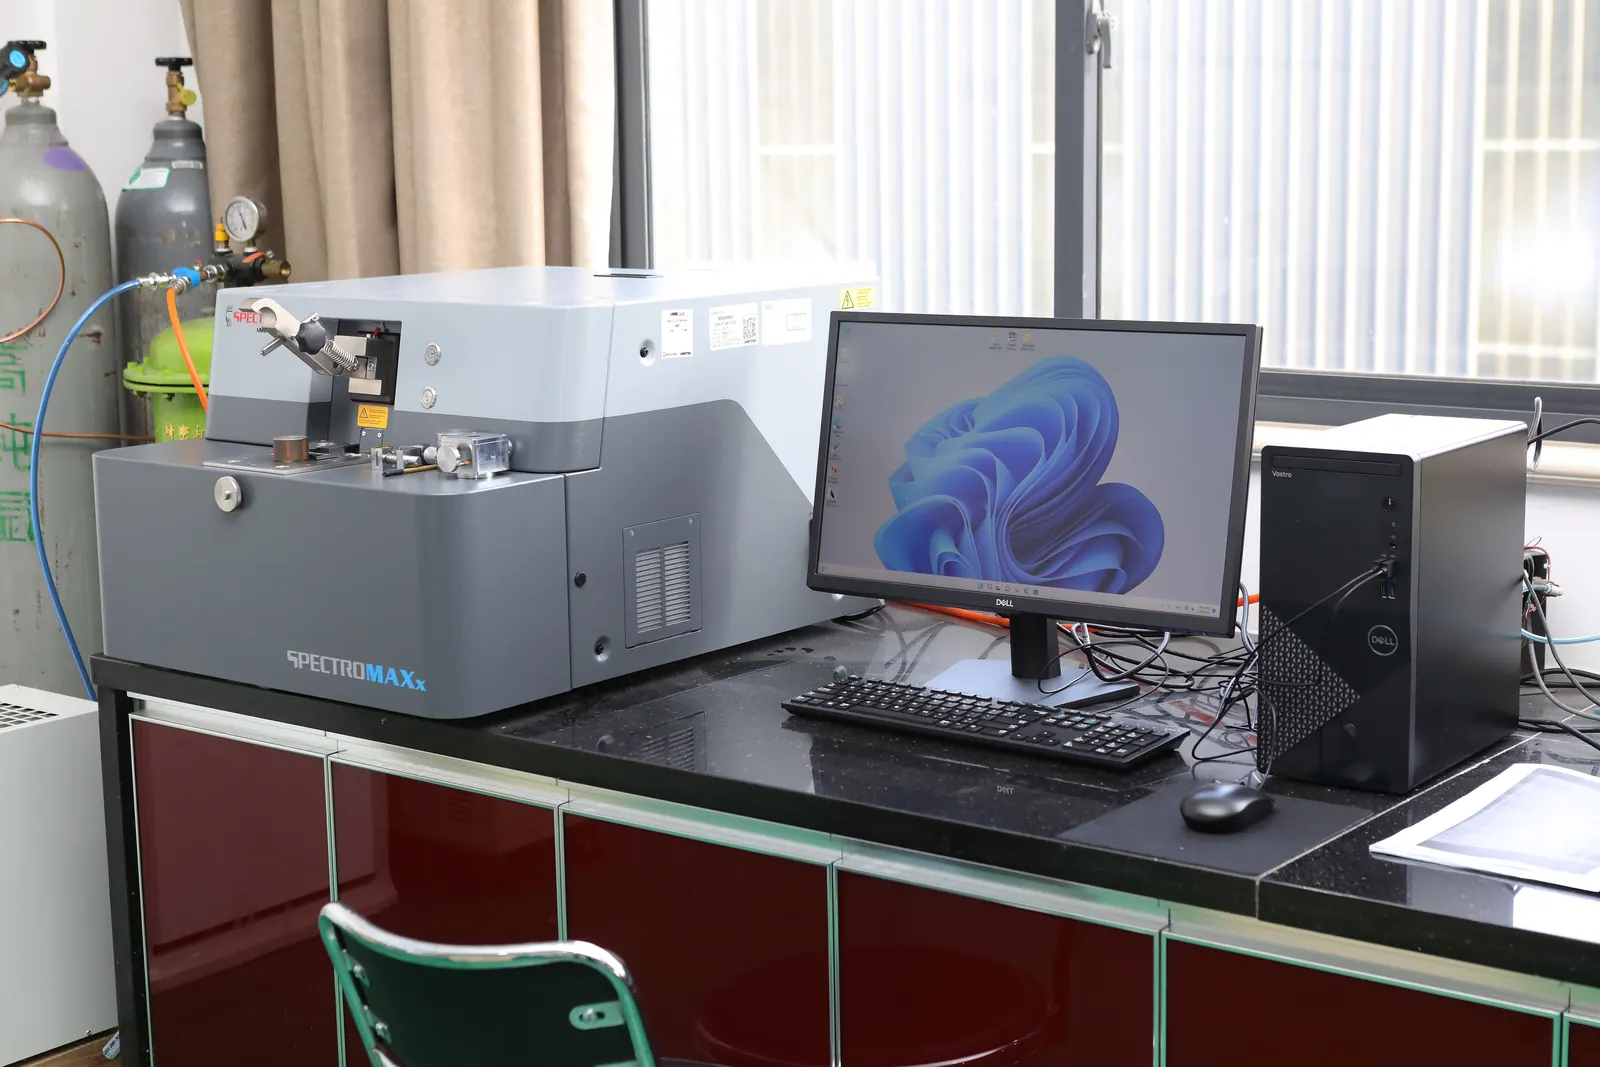
Material-analysis equipment in the measurement laboratory.
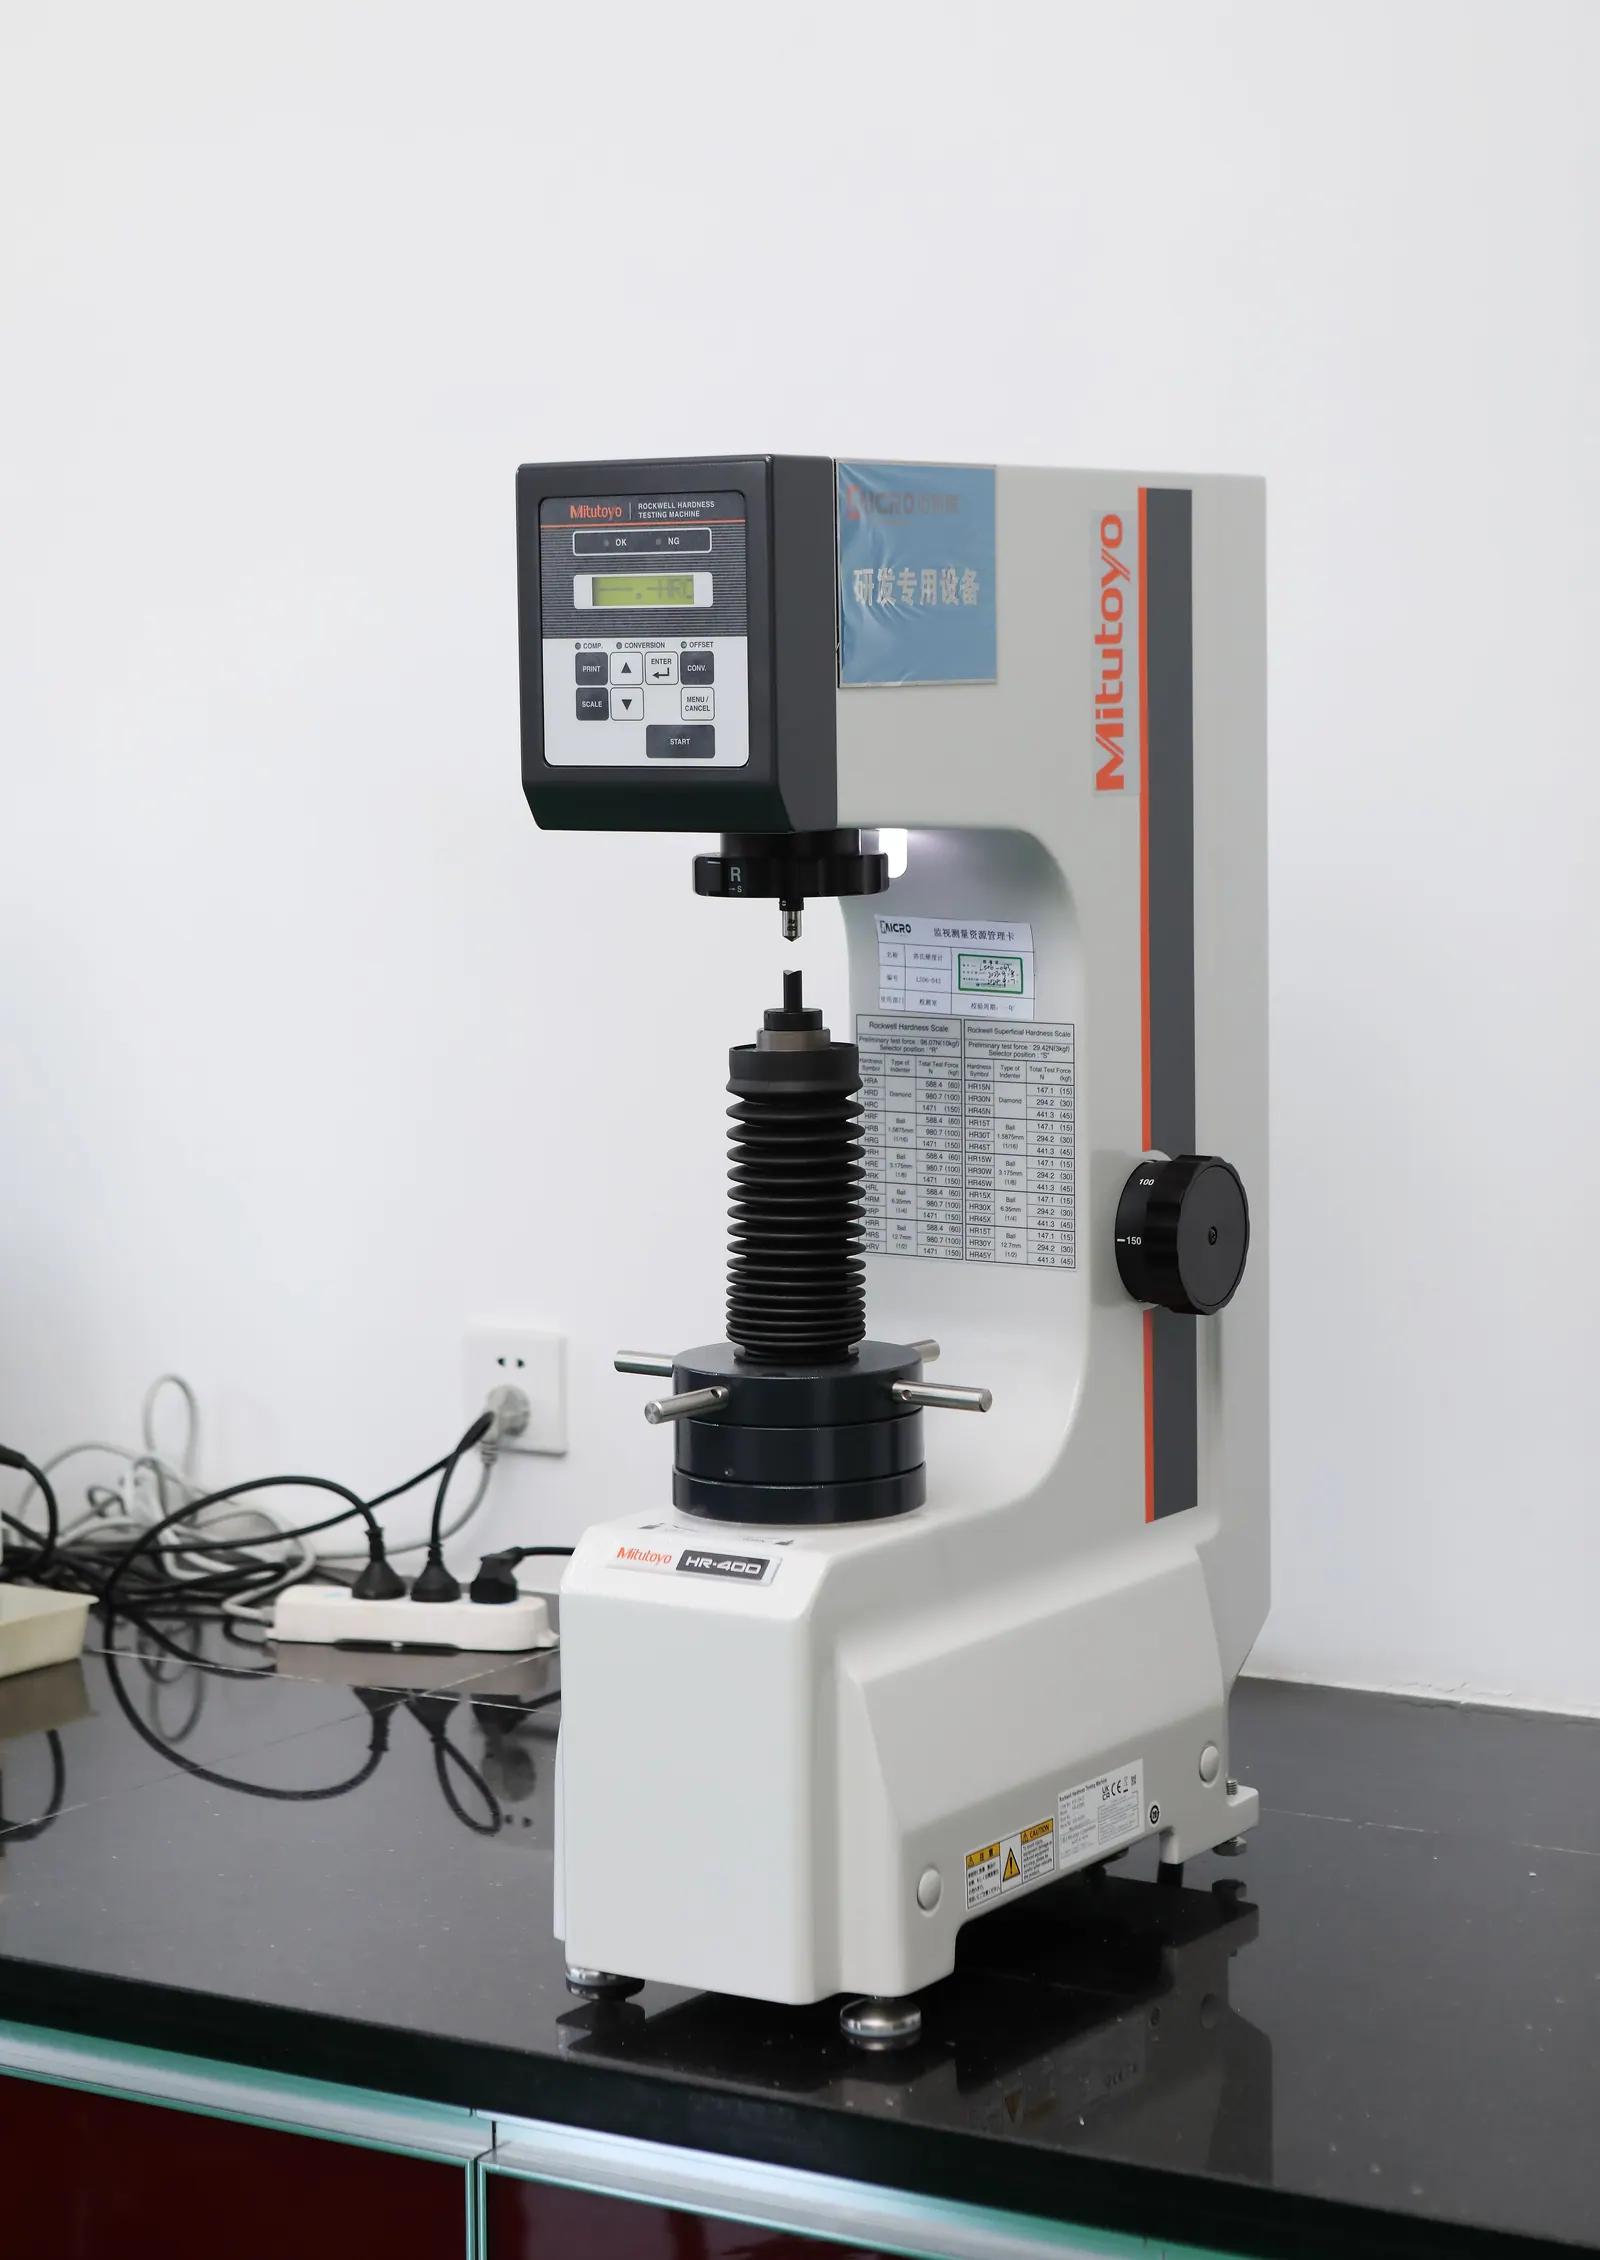
Hardness checks according to the specified material and treatment requirements.
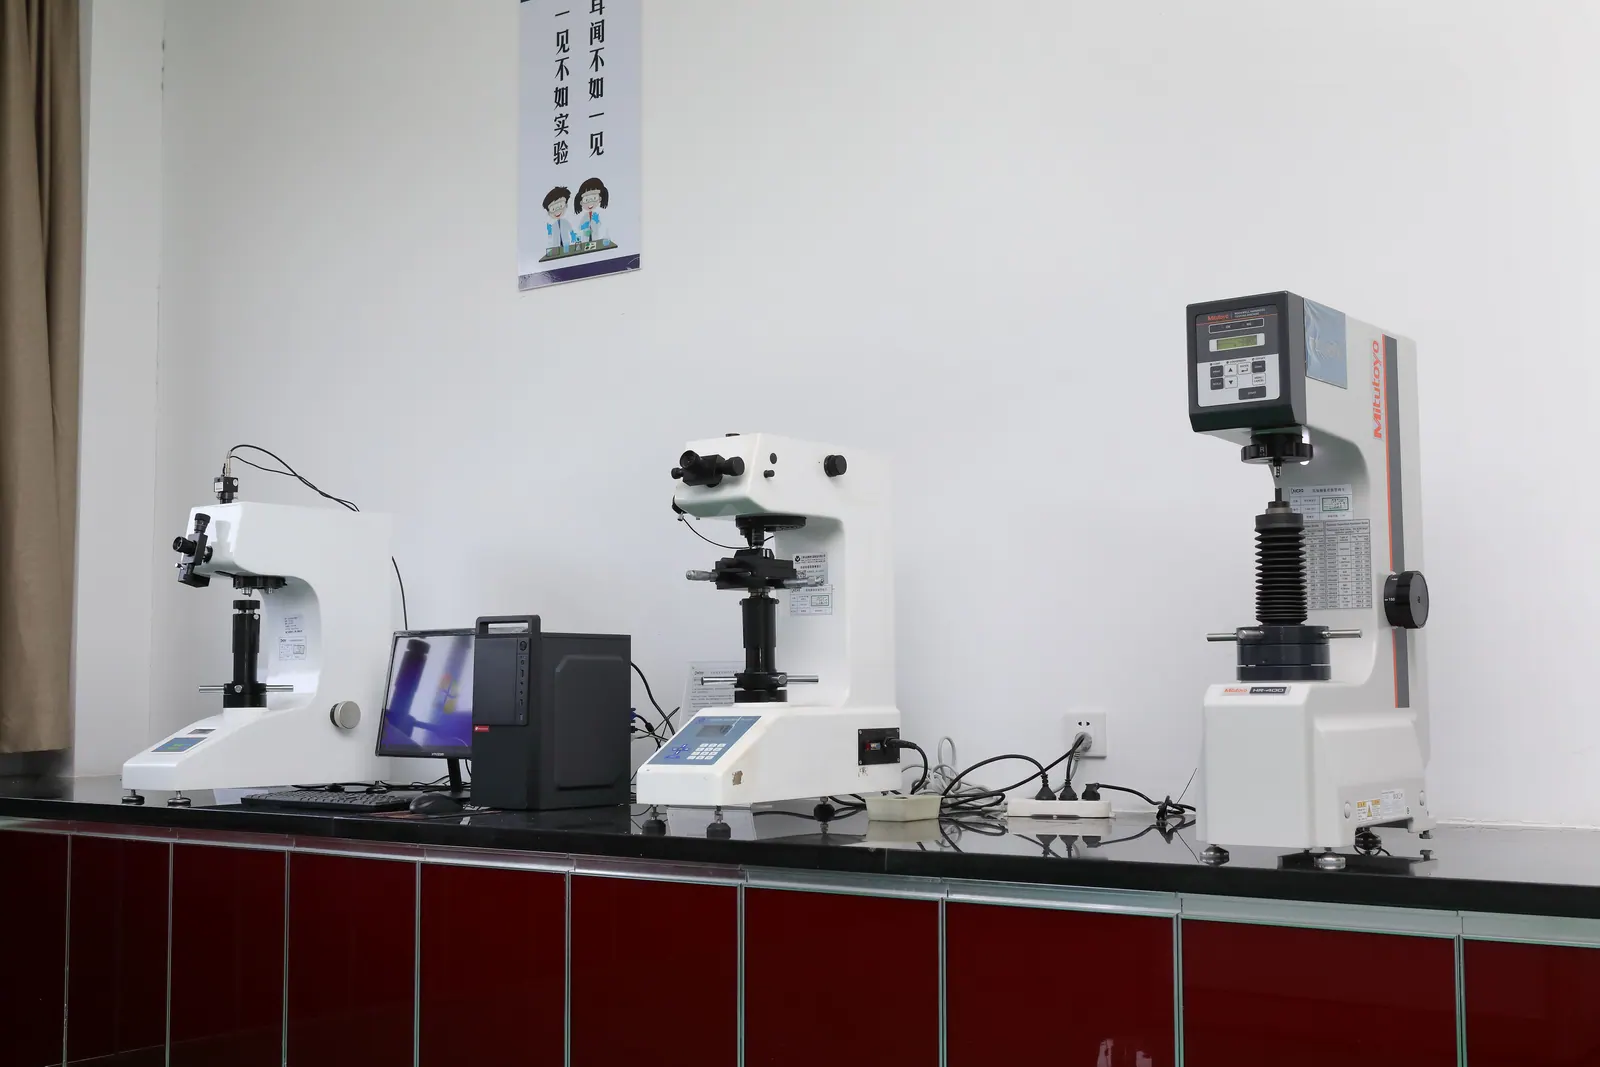
A view of the laboratory hardness-testing workstations.
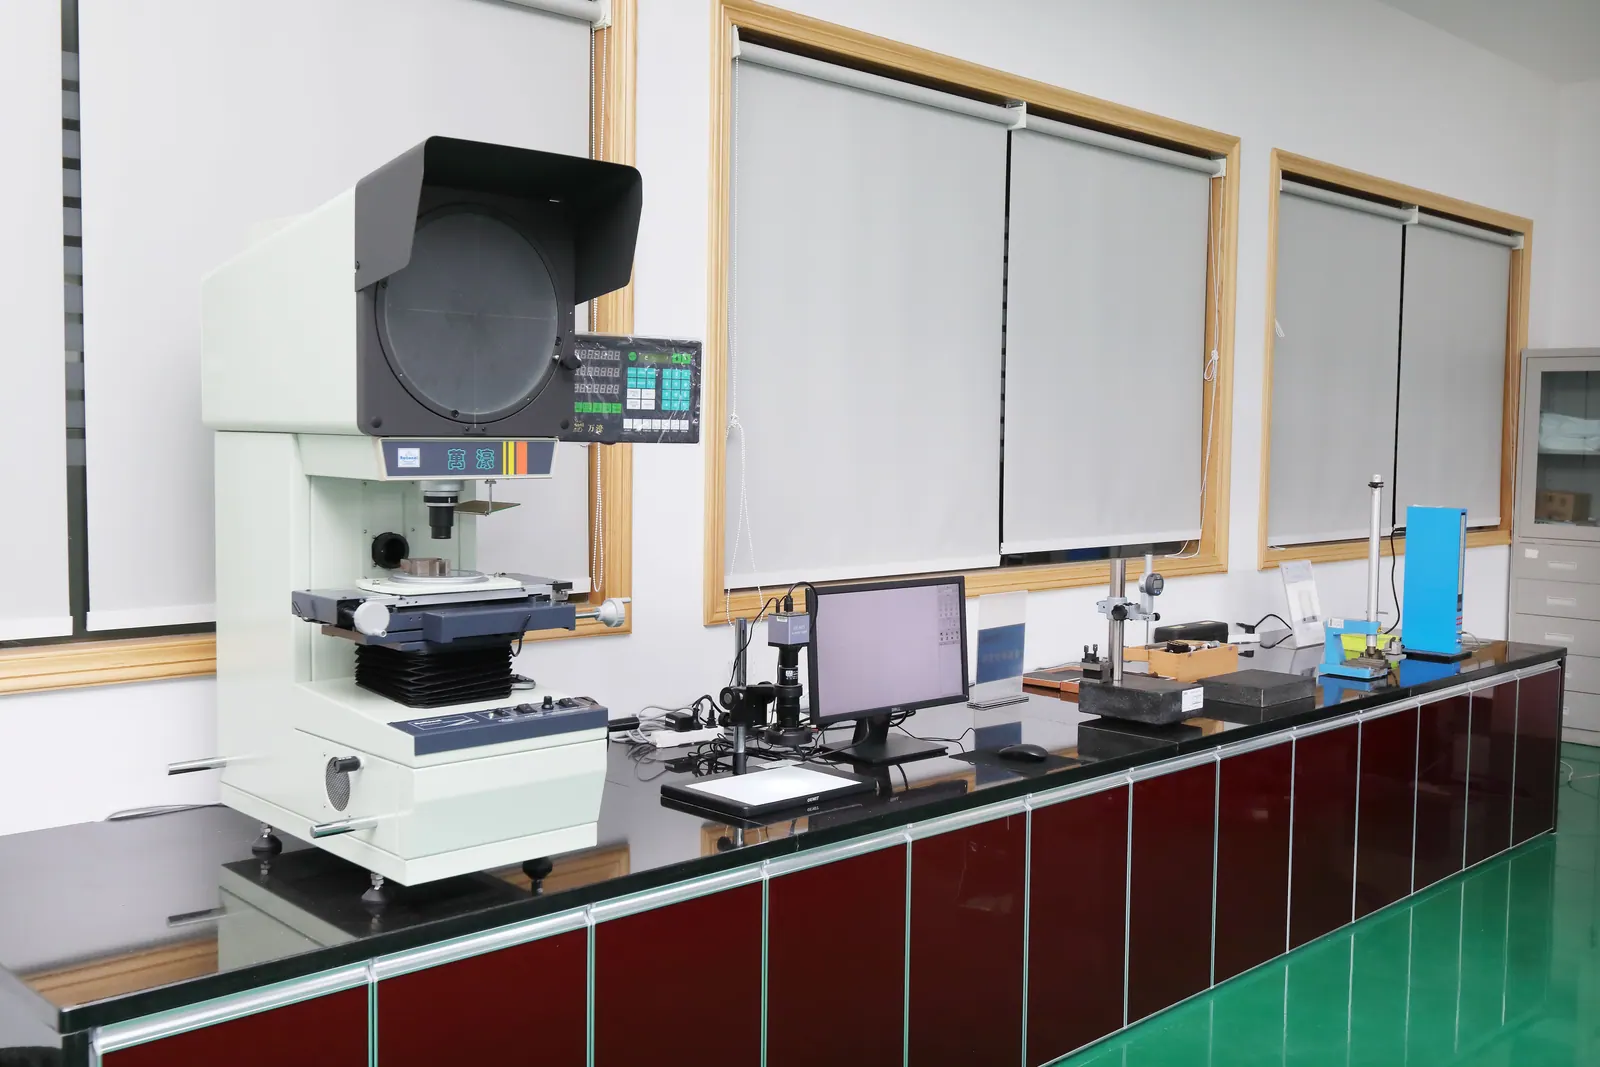
Optical comparison of component profiles and defined features.
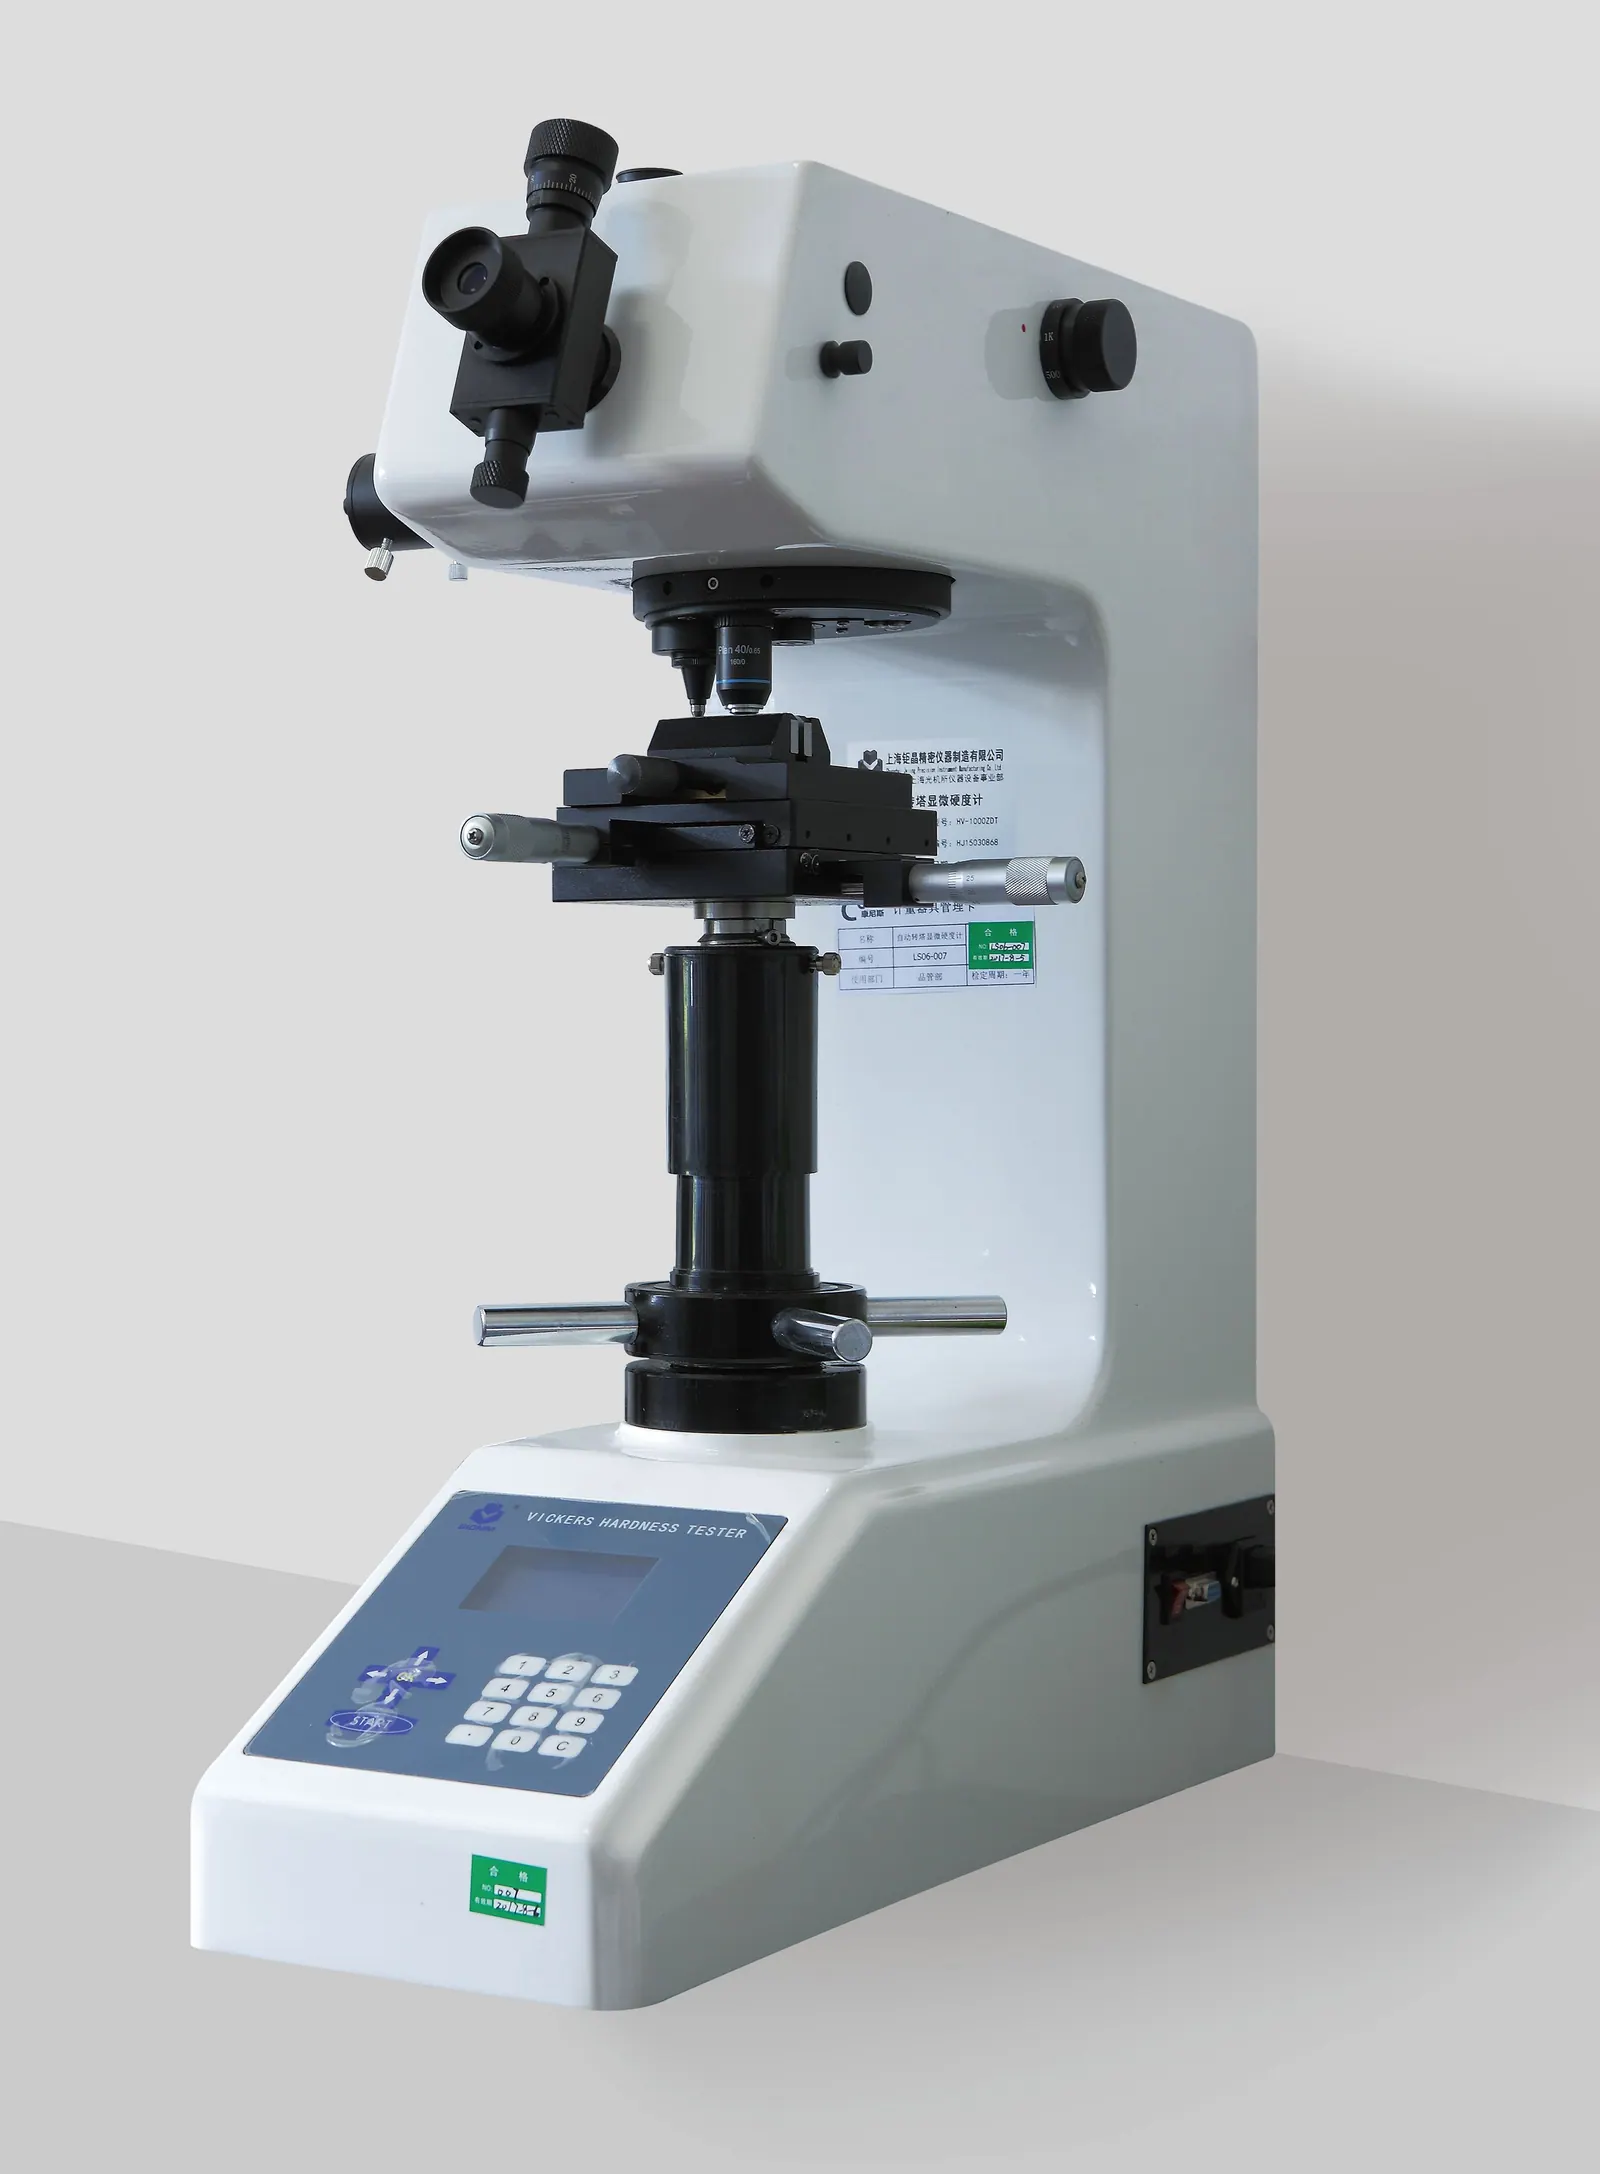
A closer view of a laboratory hardness-testing instrument.
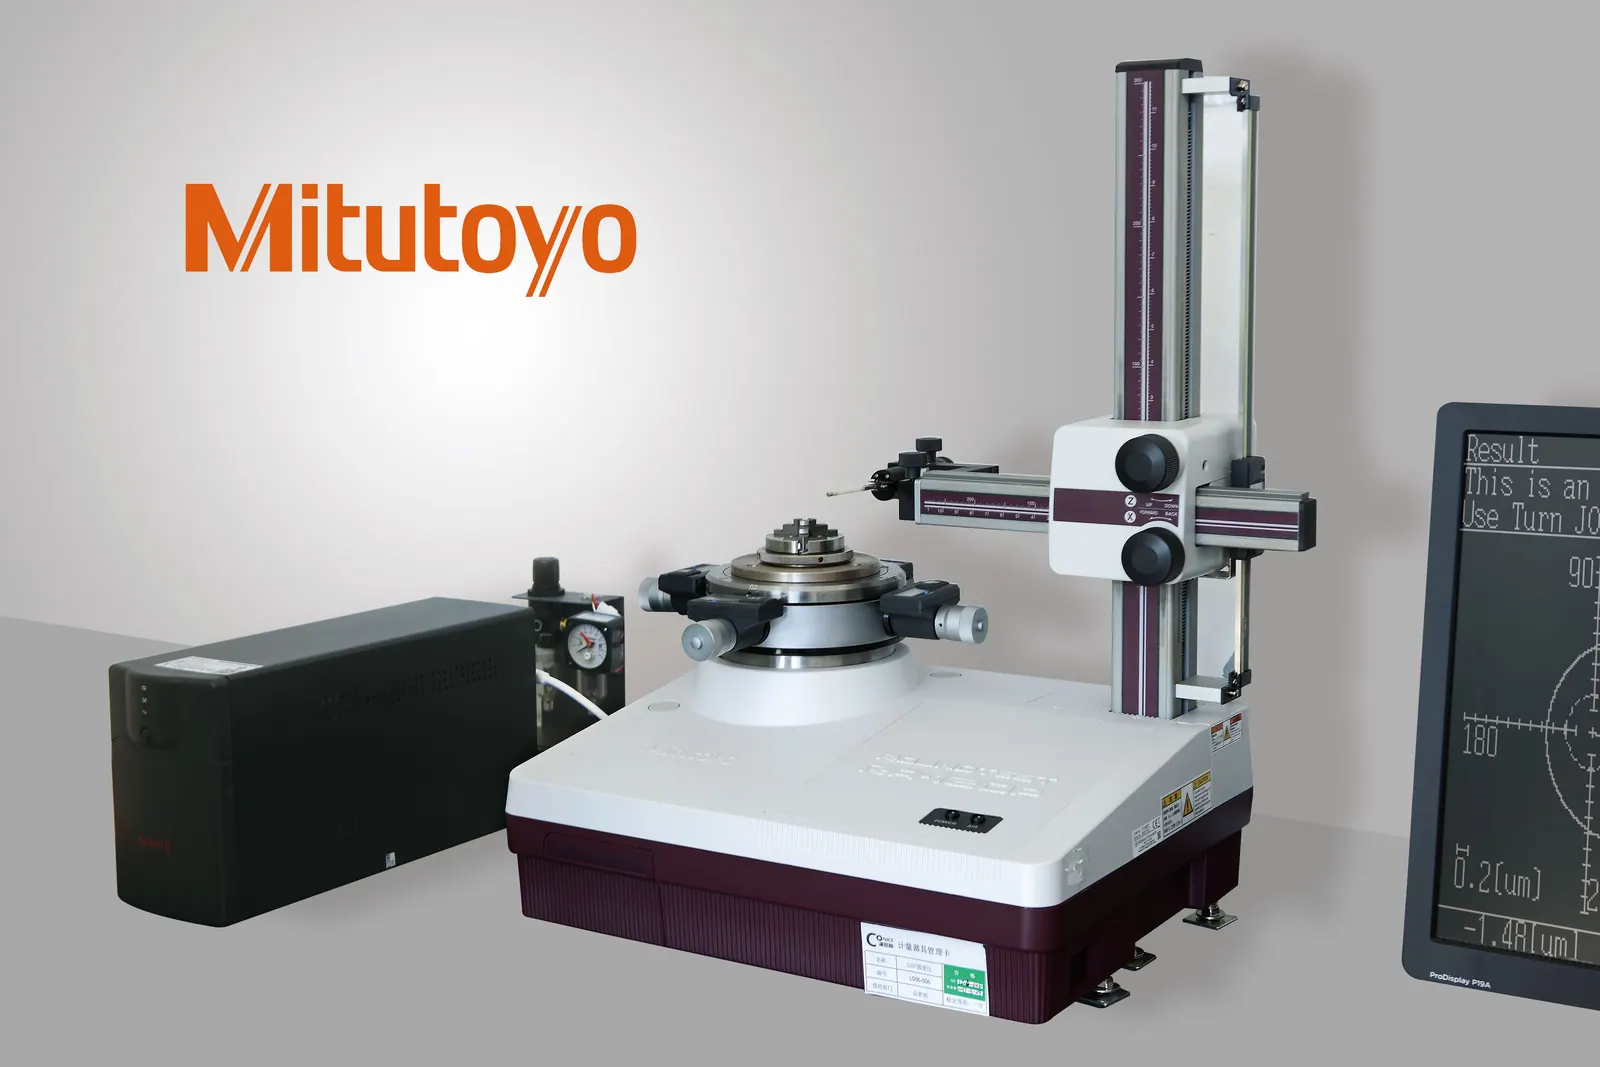
Roundness measurement of specified cylindrical features.
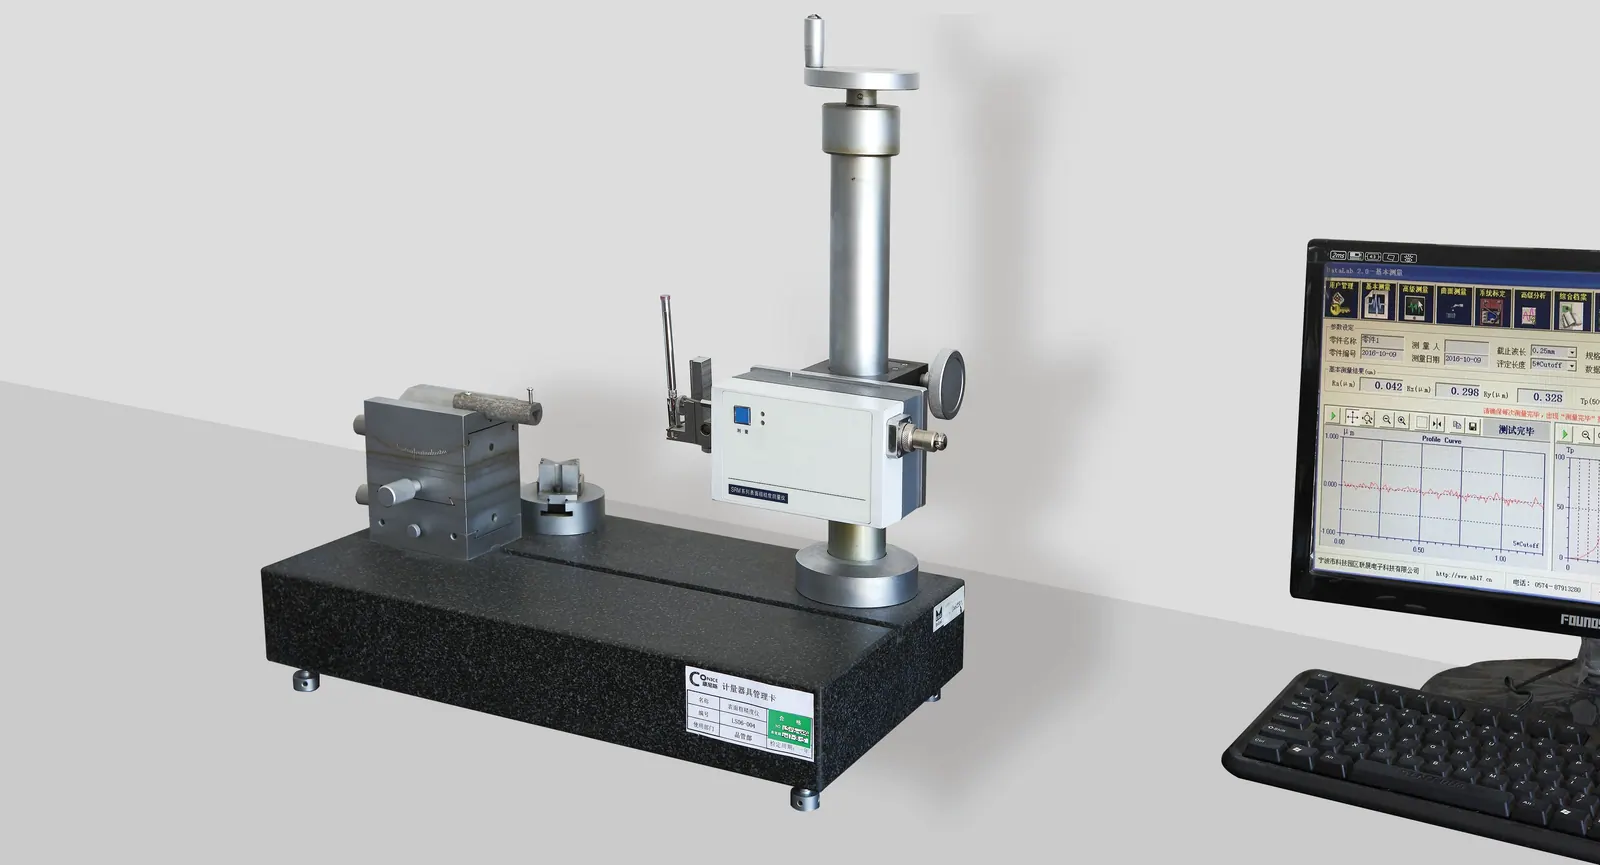
Surface-texture measurement at the locations defined in the inspection plan.
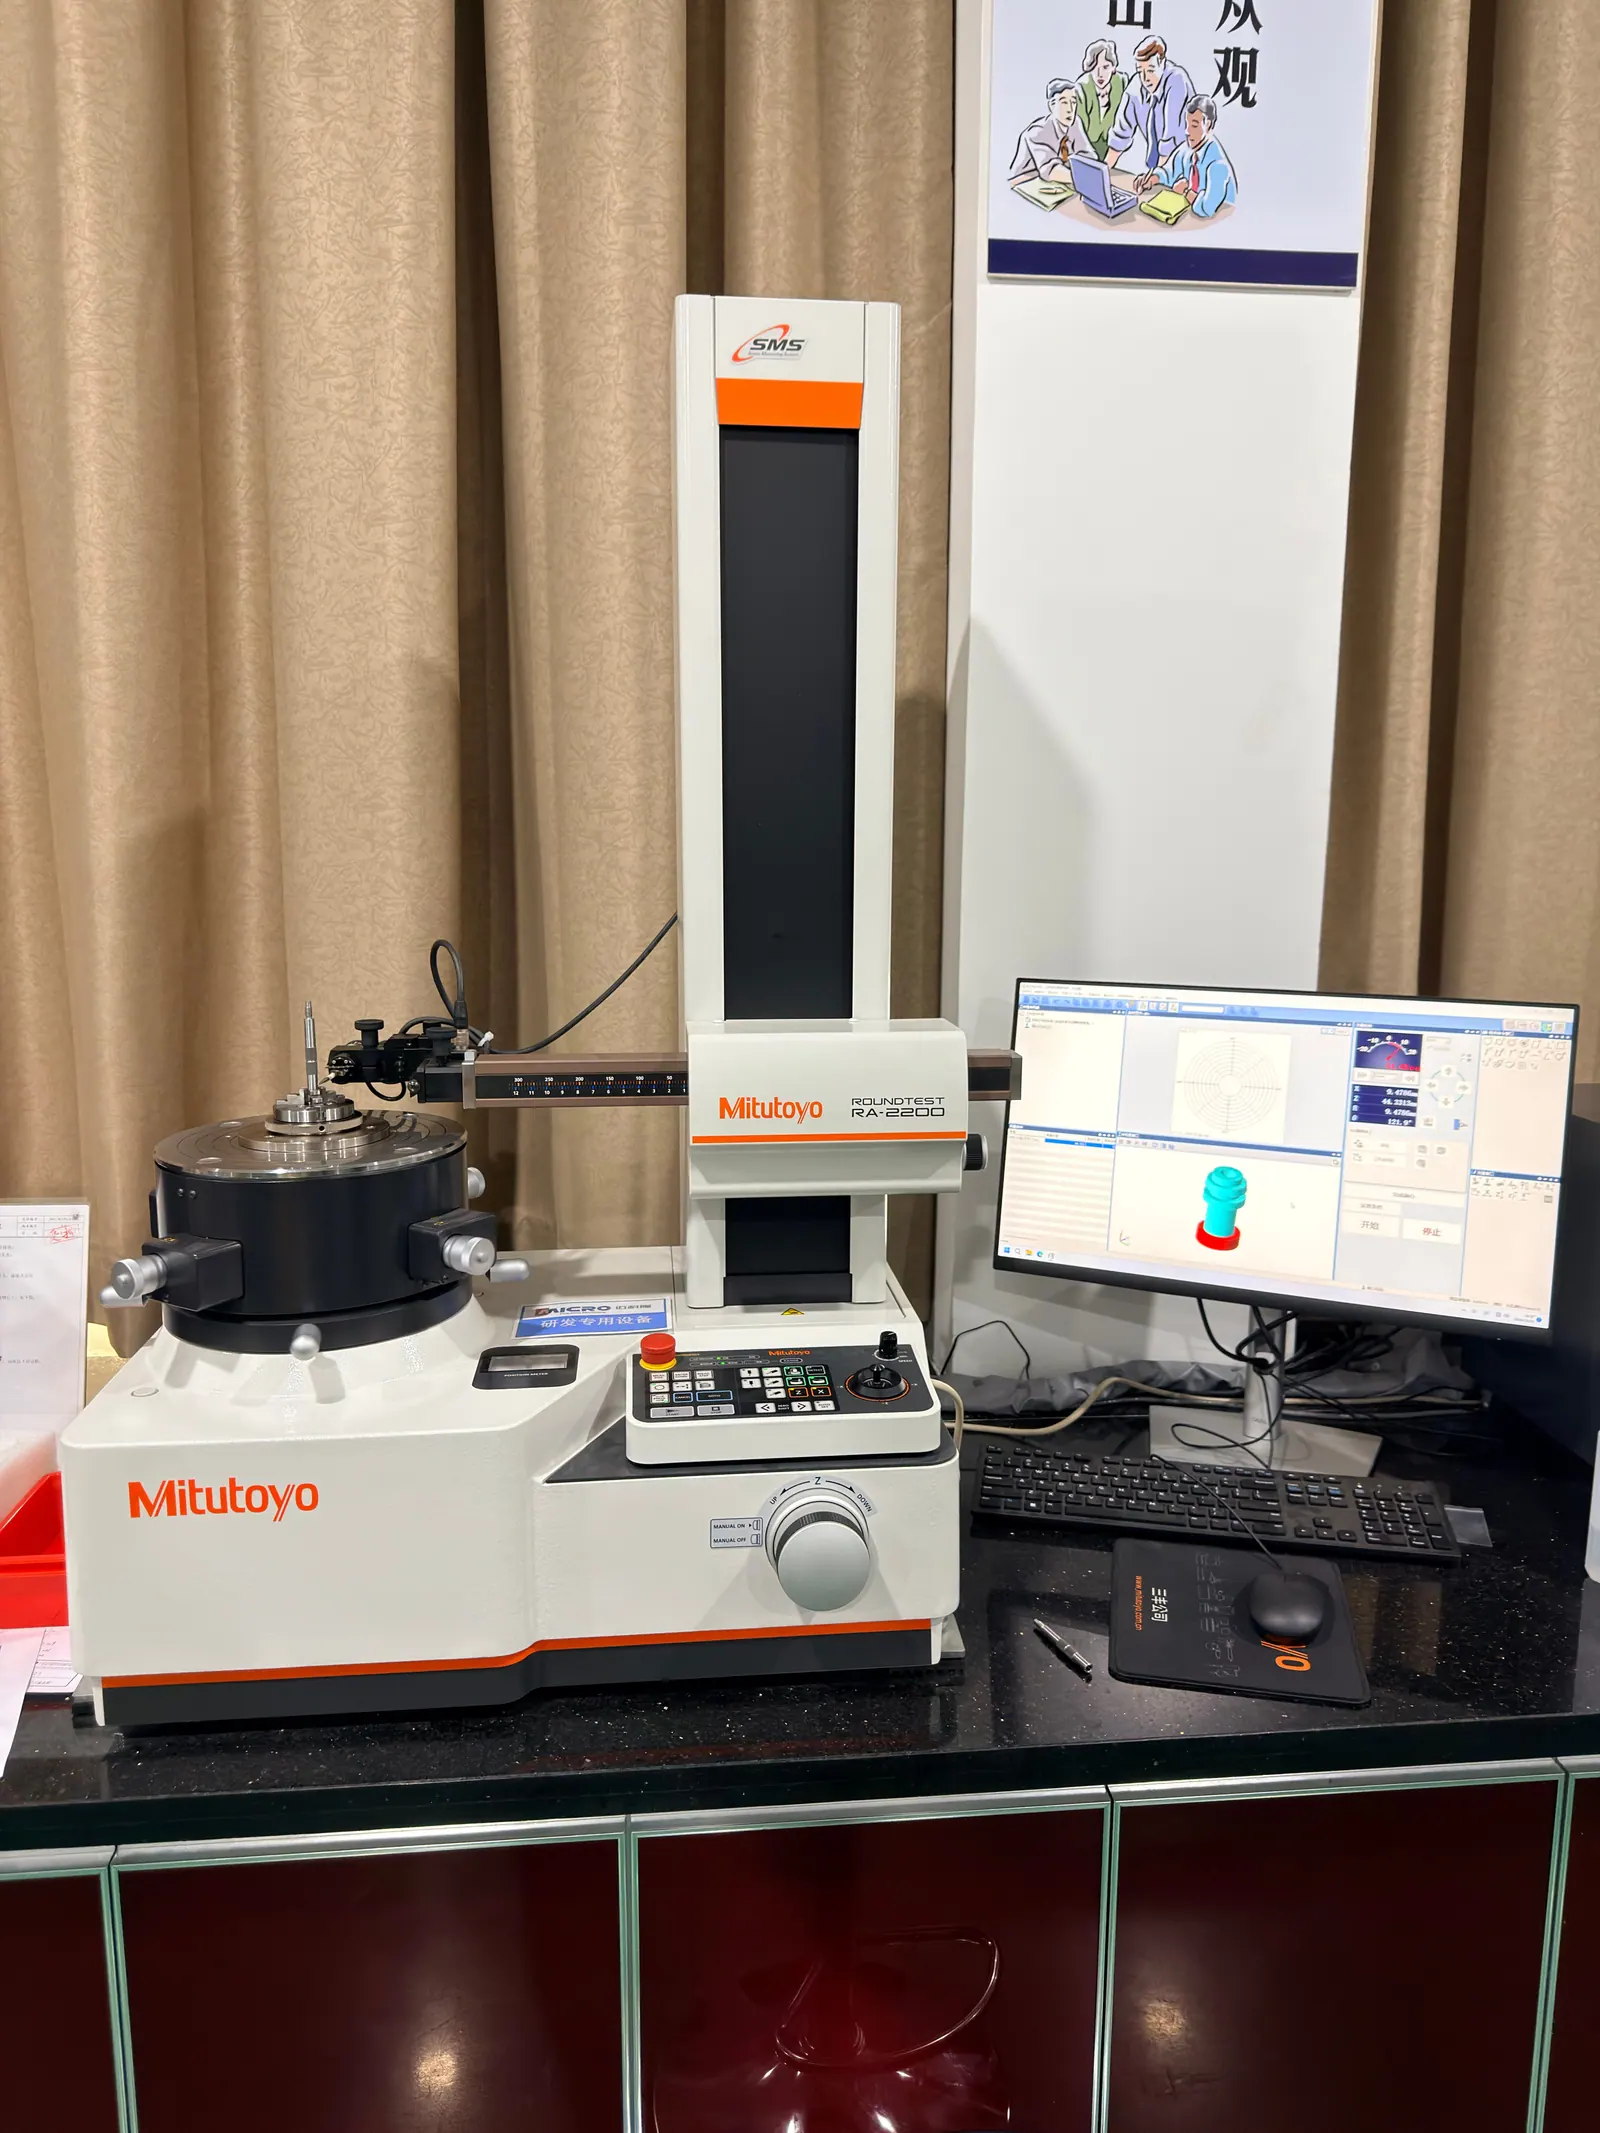
Instrument setup for checks of specified cylindrical geometry.
Component checks and additional views from the measurement laboratory. Select a photograph to see the full view.
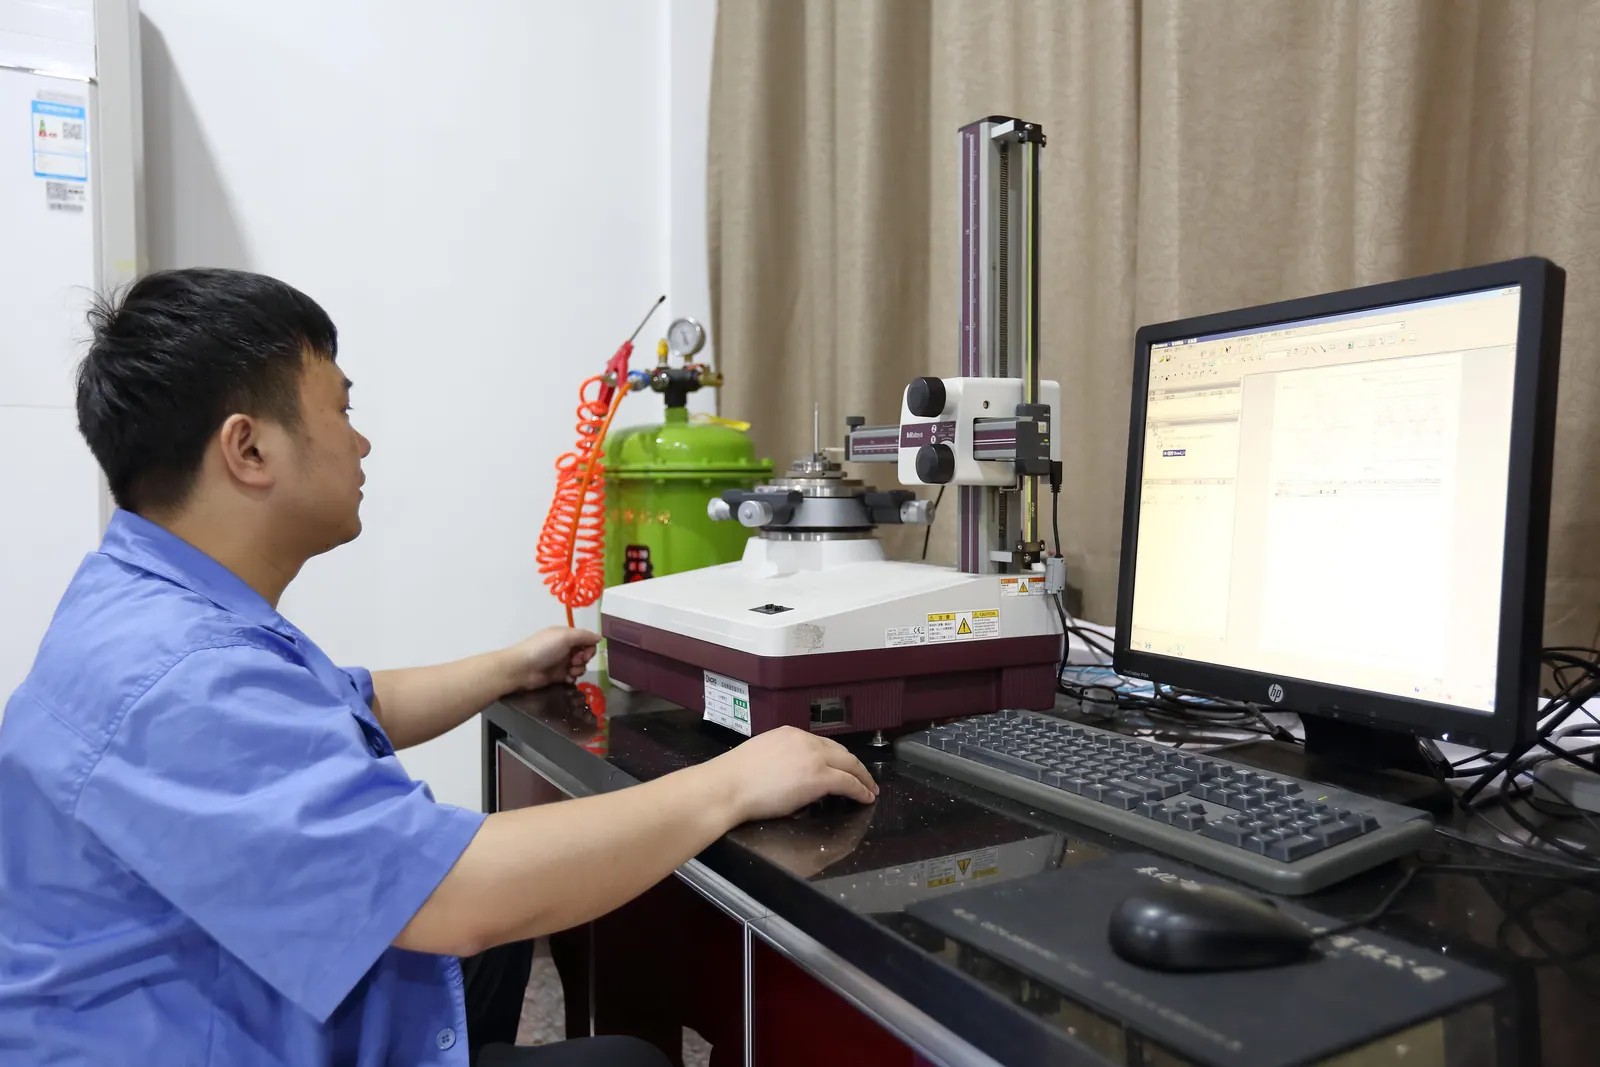
An operator measuring a component in the inspection laboratory.
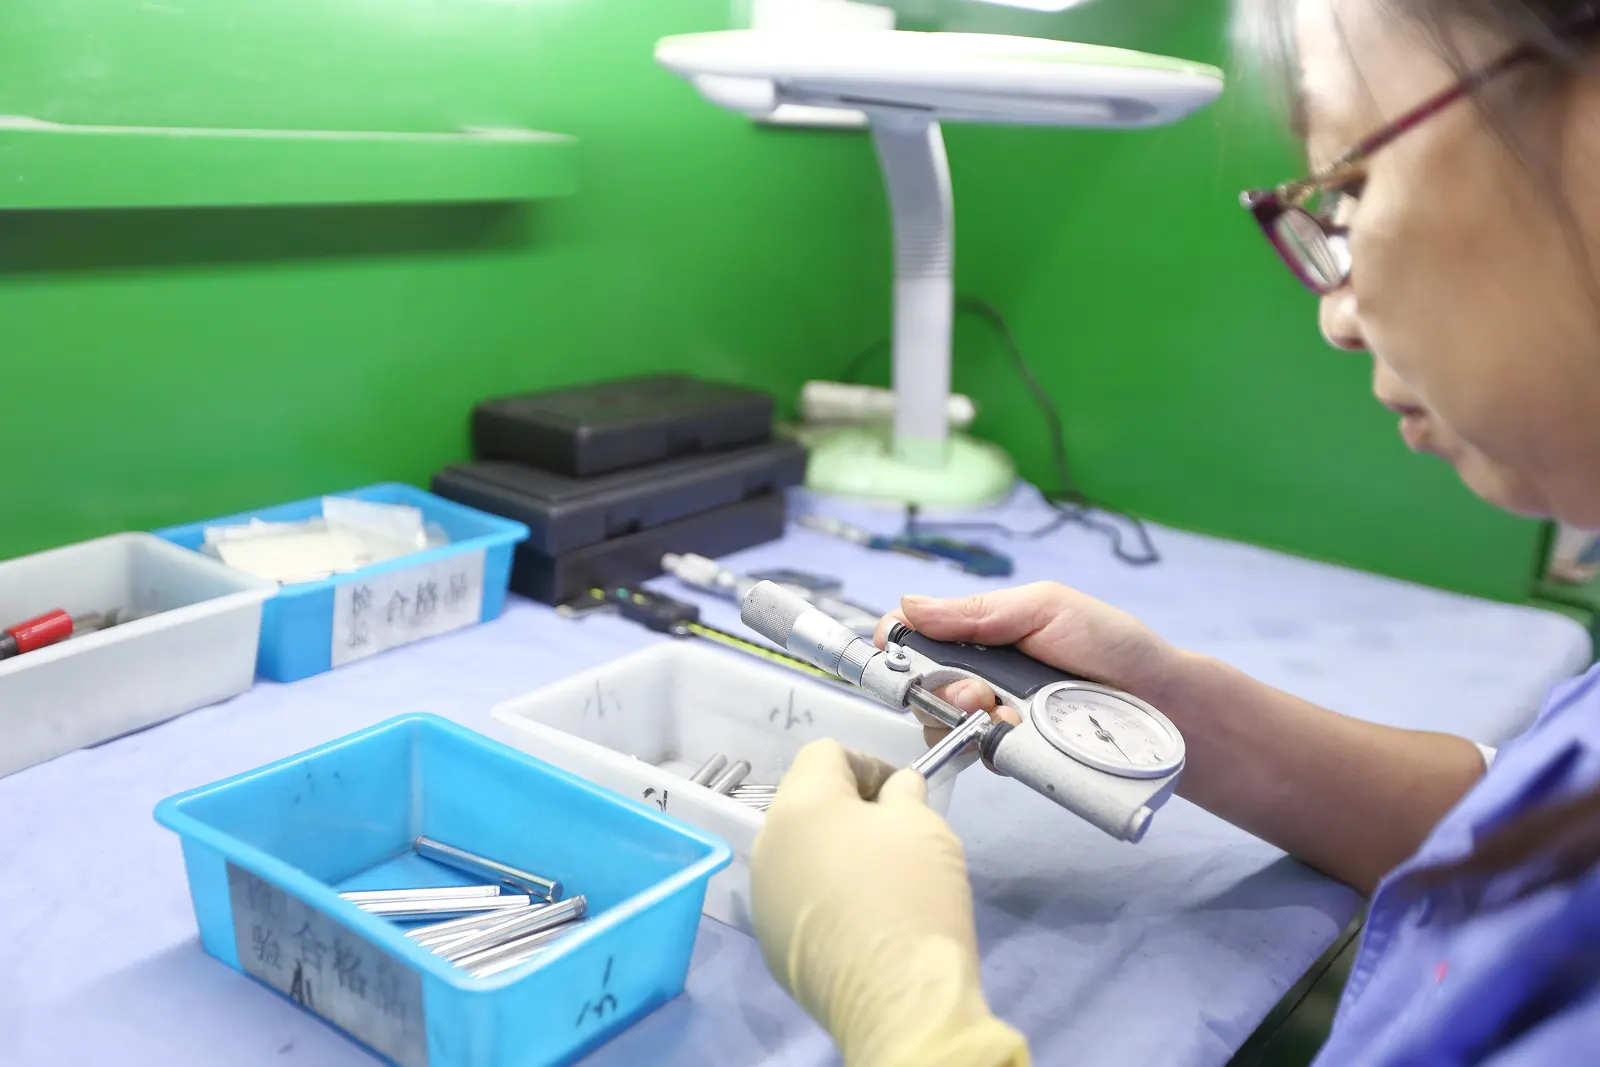
Diameter checks at the defined measurement locations.
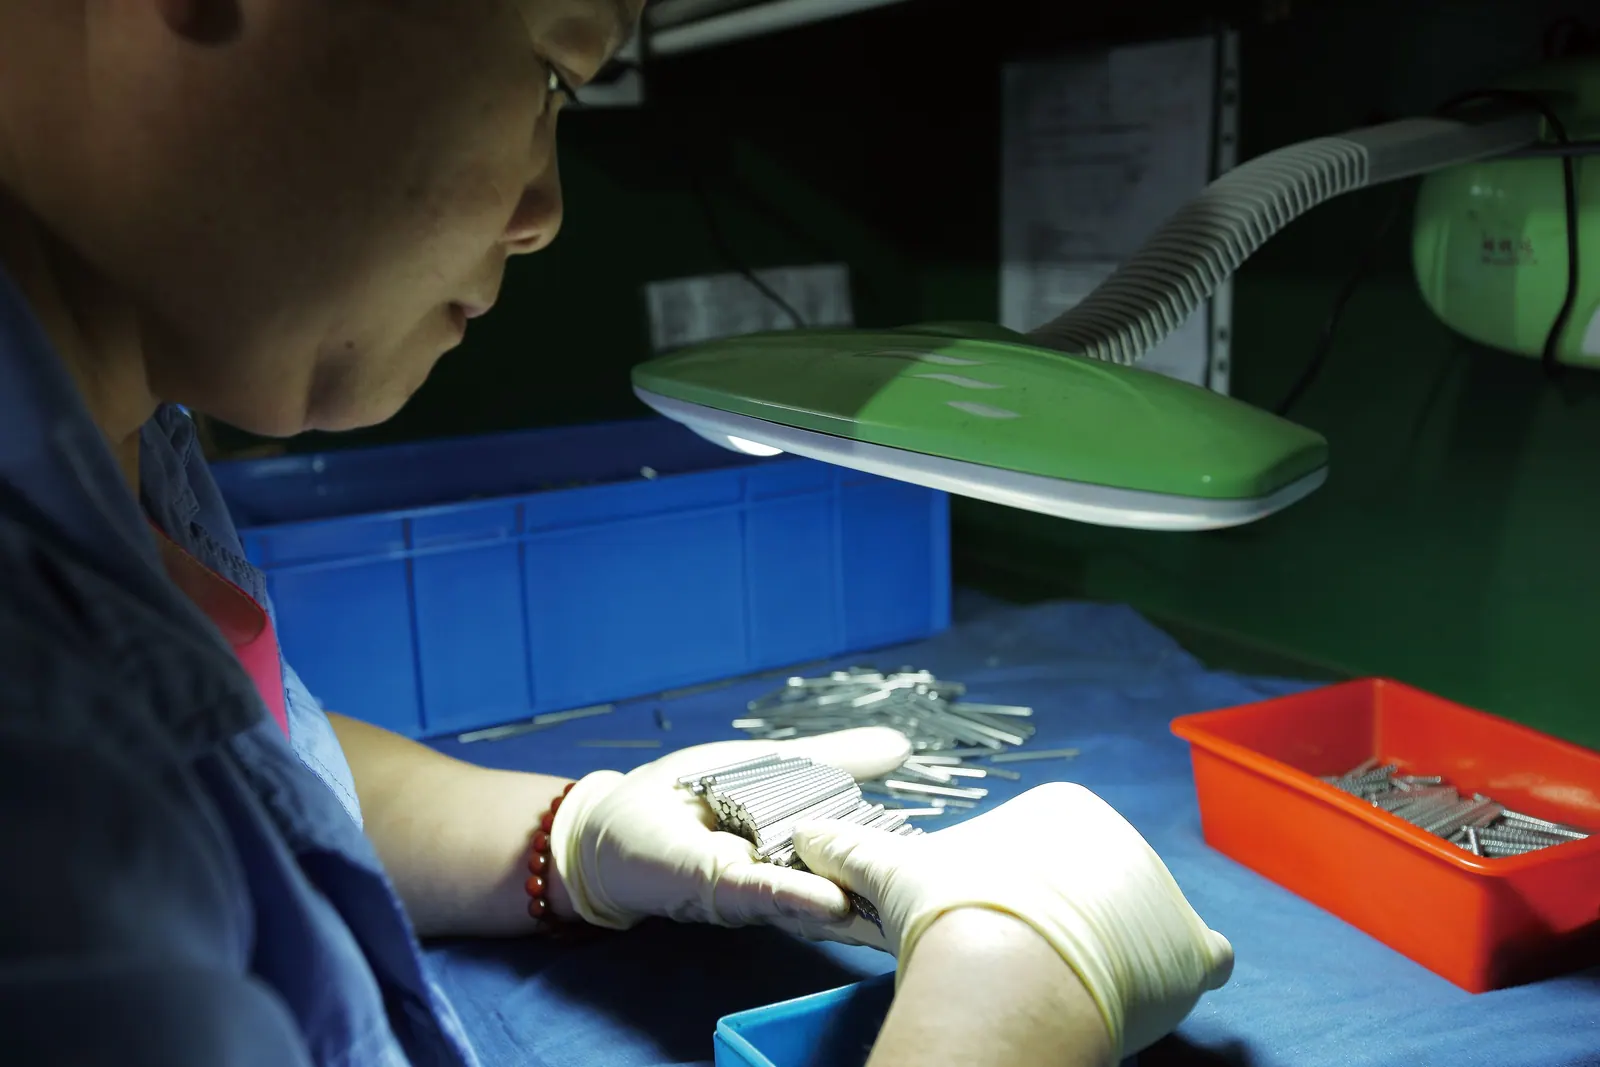
Visual inspection of parts at an illuminated work station.
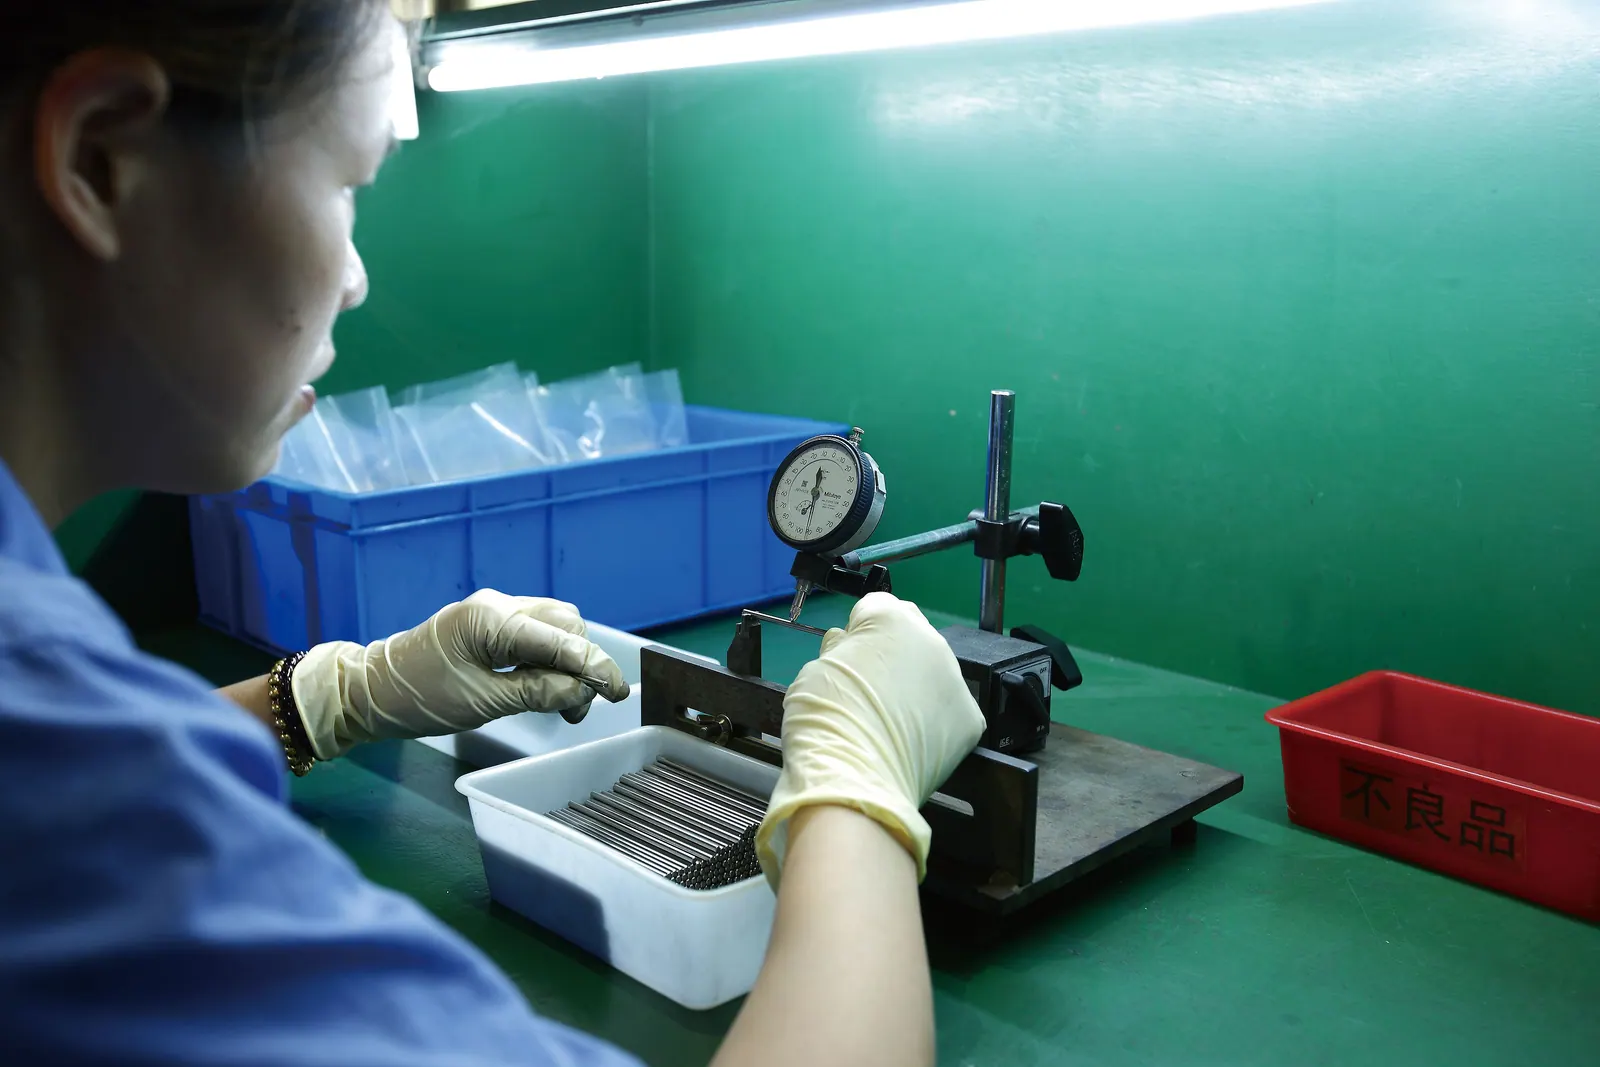
Checking a component with a dial indicator and a dedicated fixture.
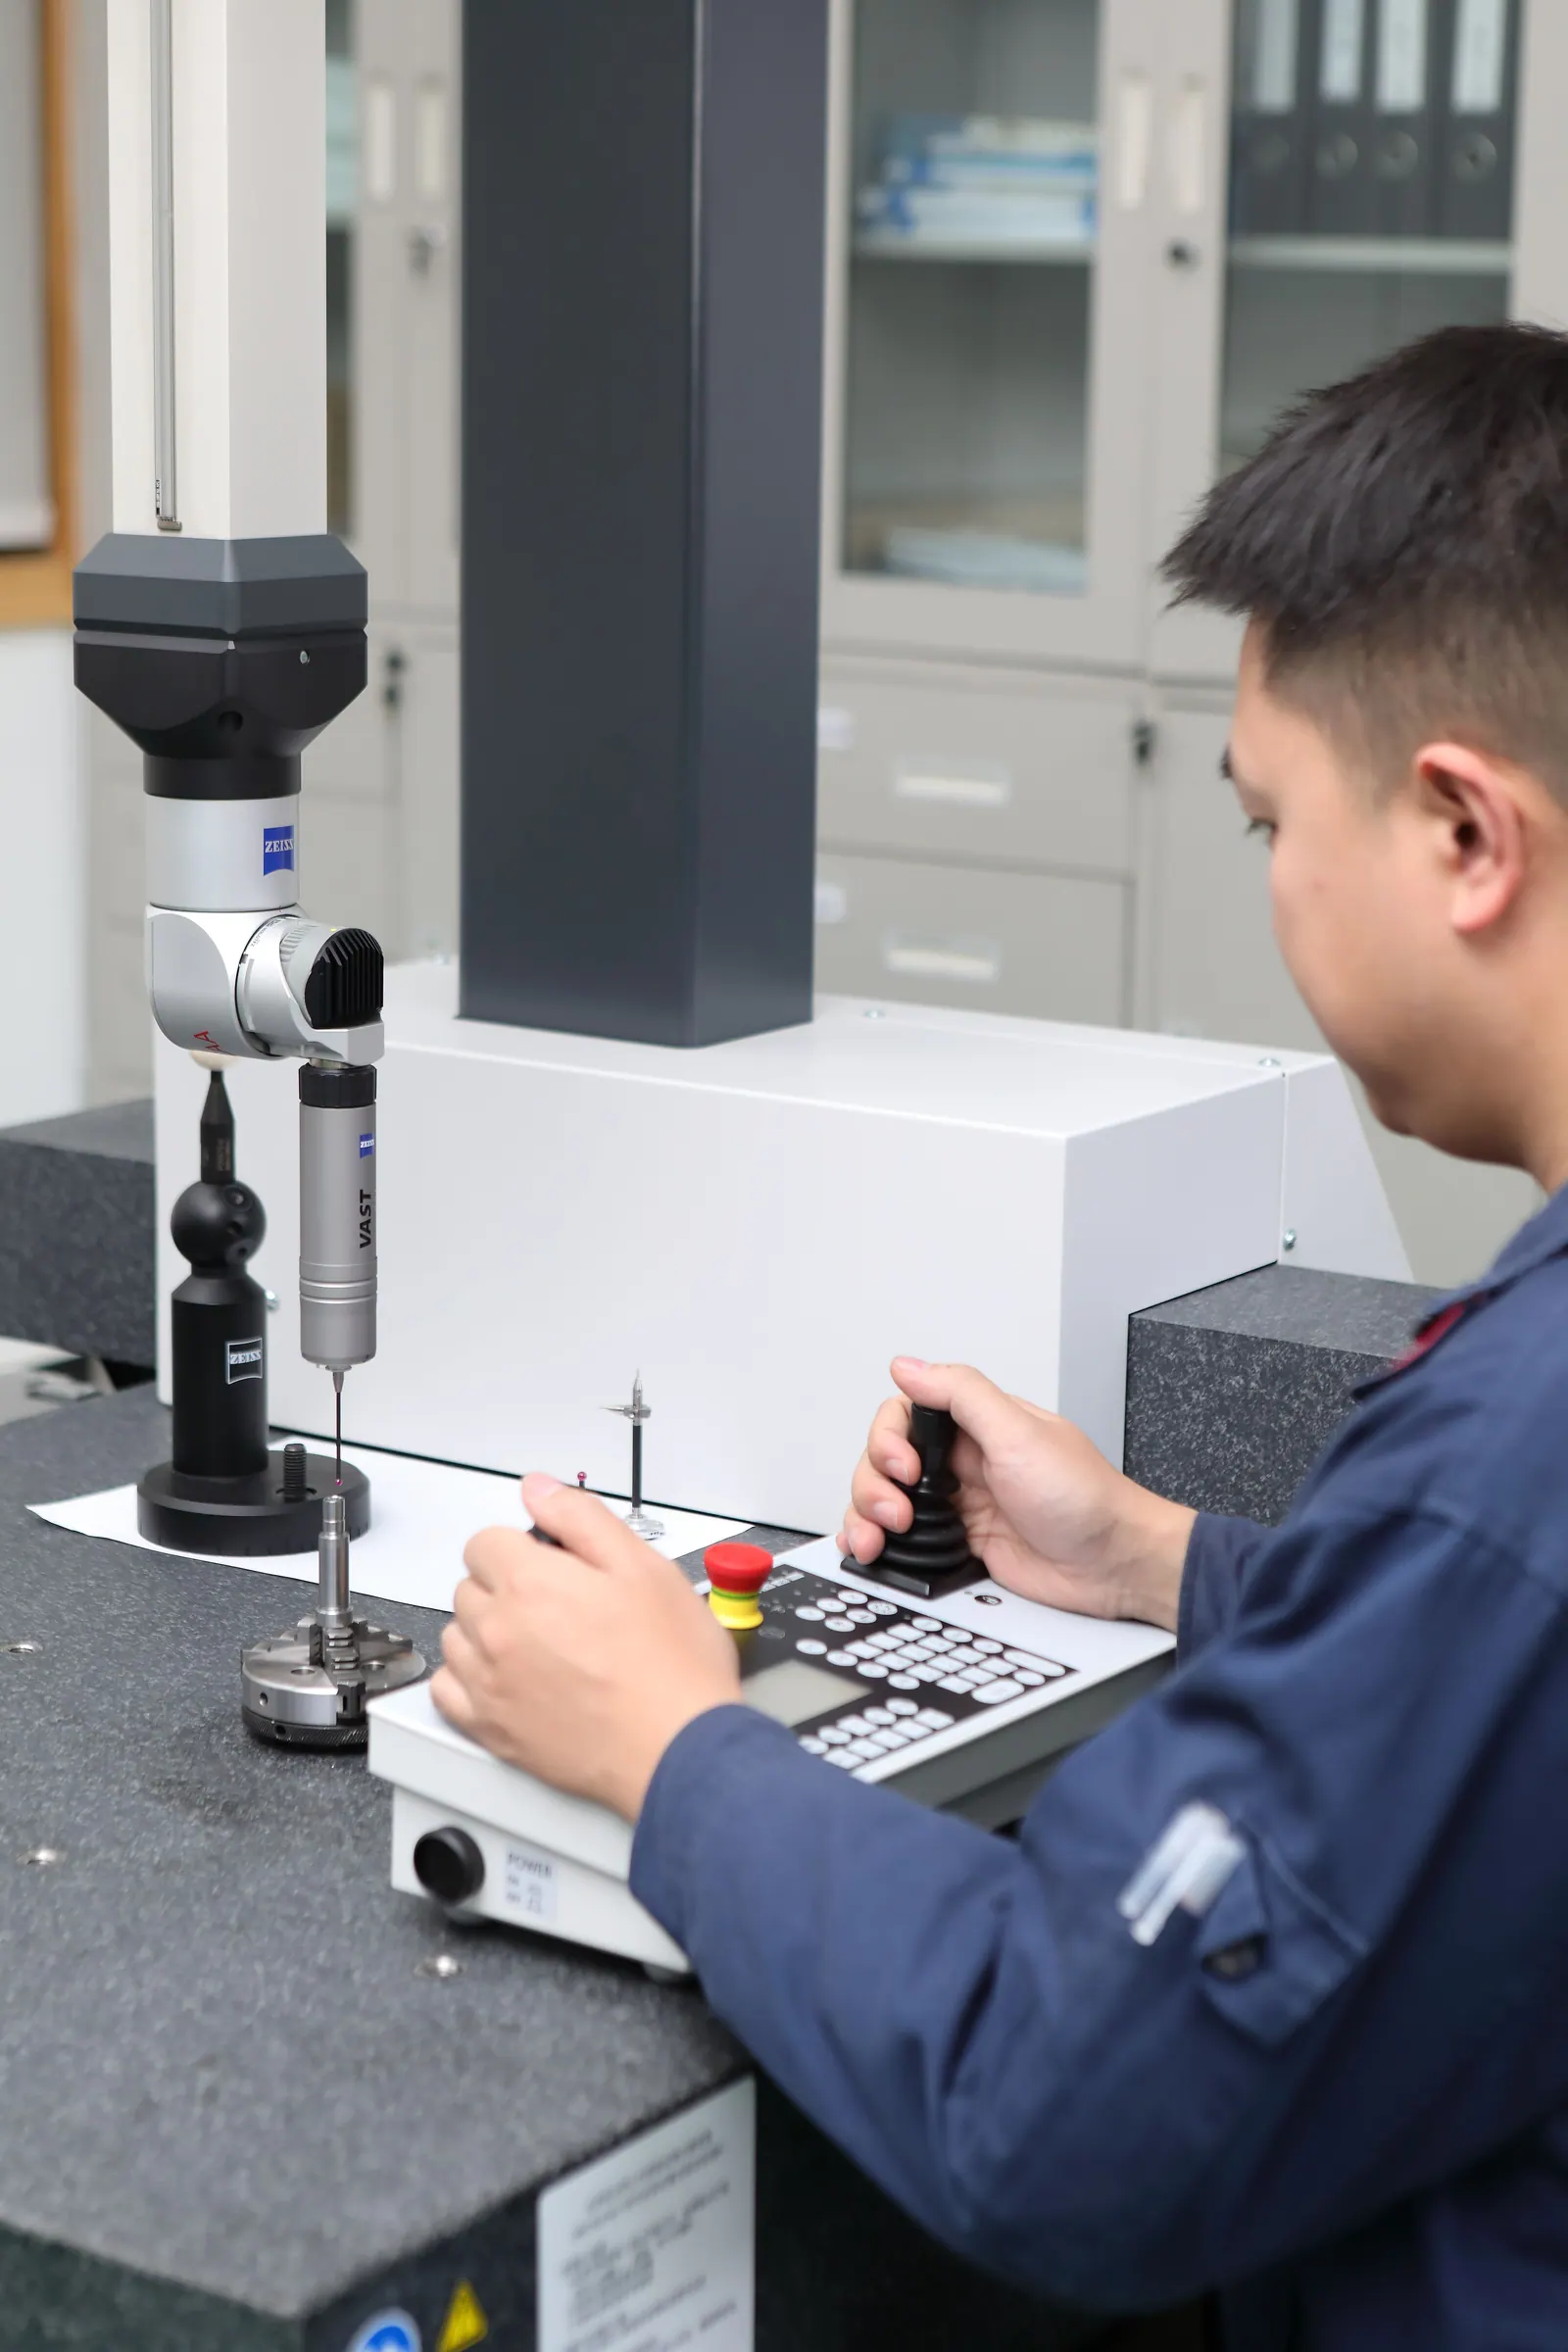
Another view of the operator and coordinate measuring machine.
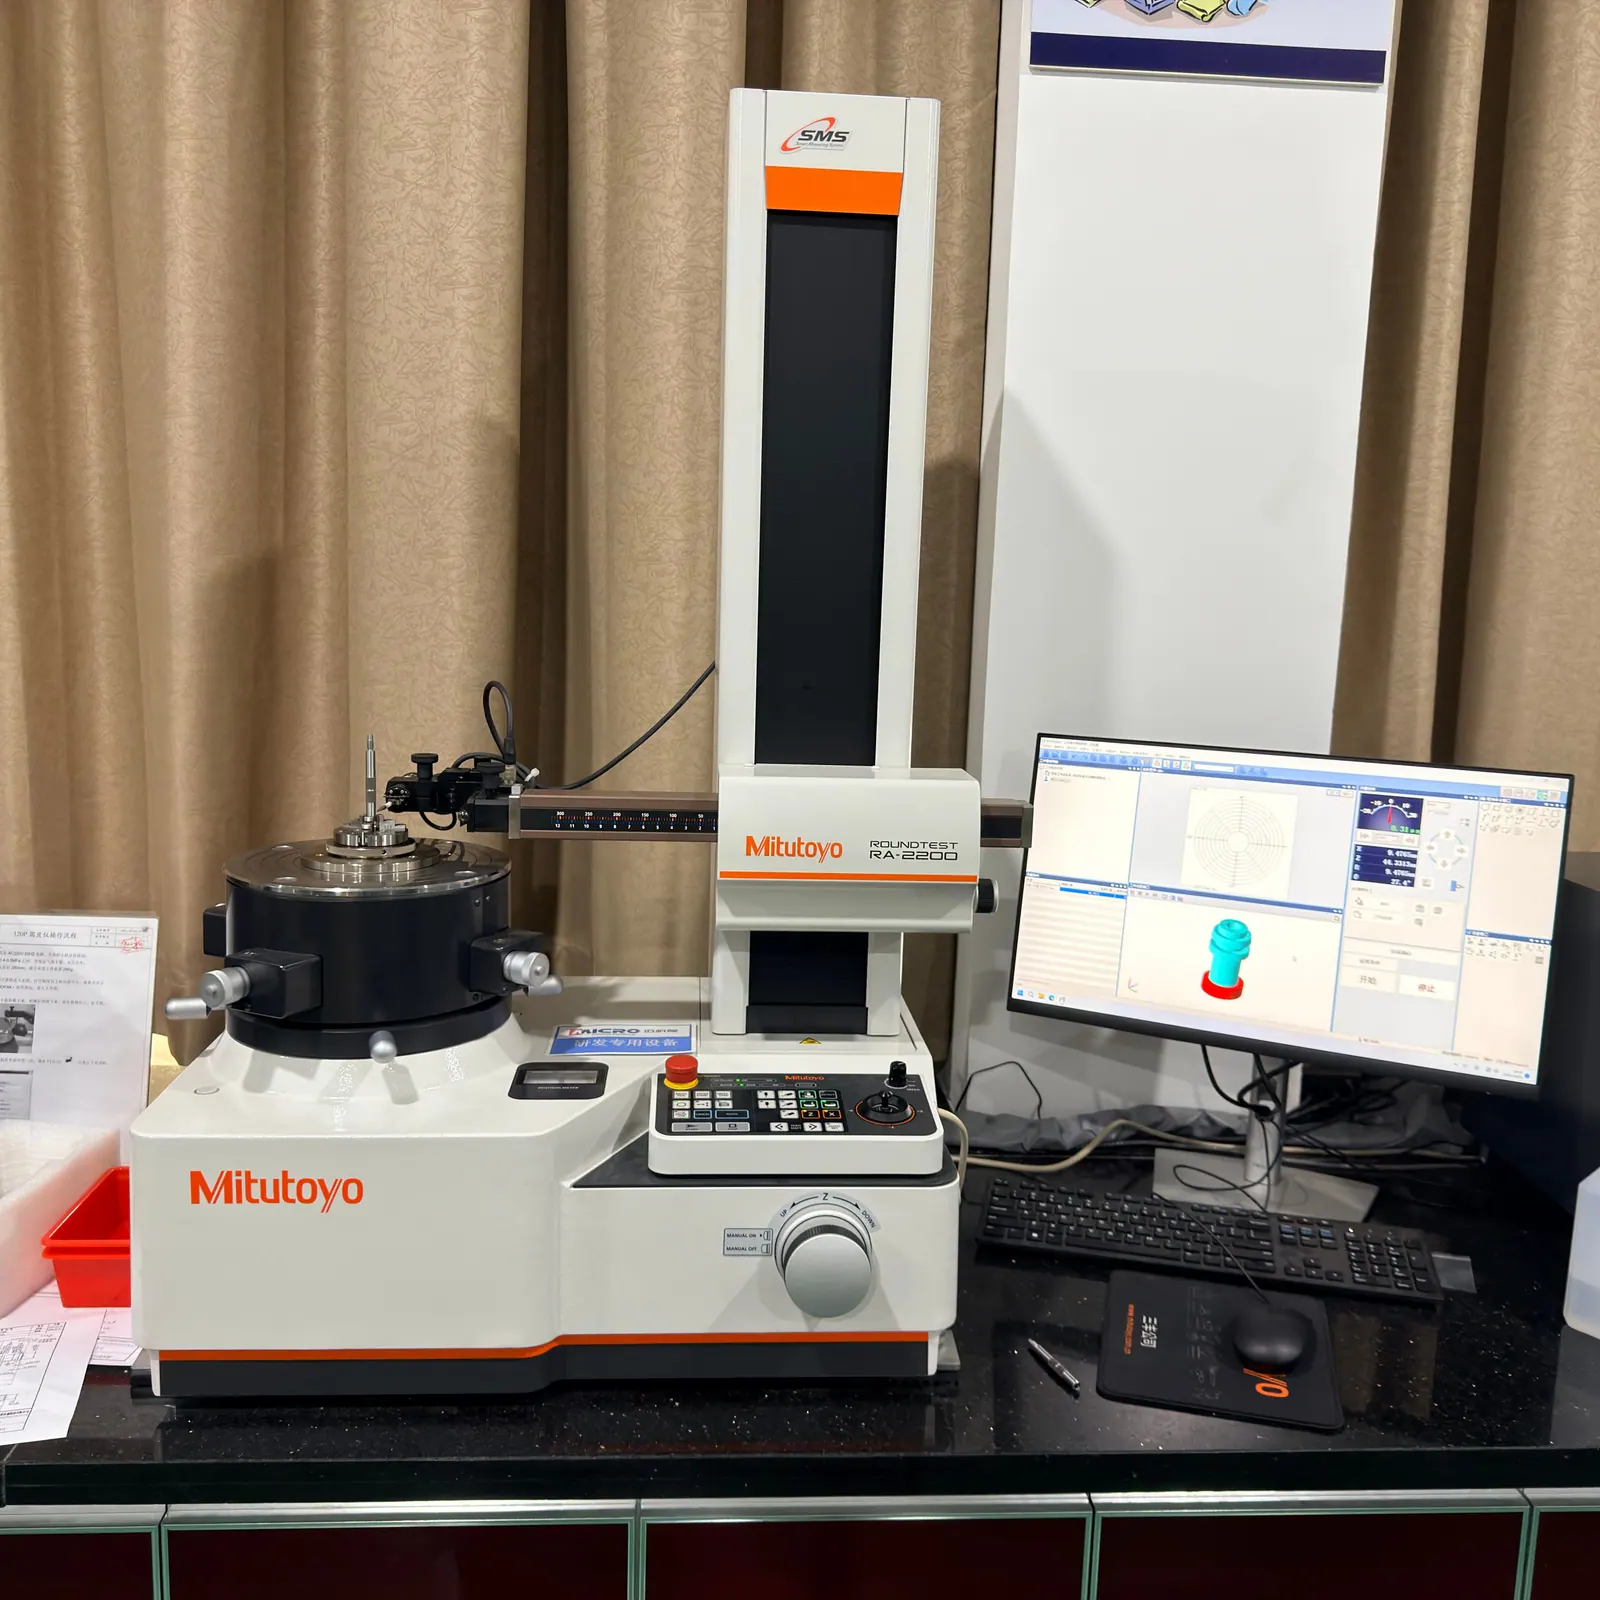
An additional view of the cylindrical-feature measurement setup.
Identify the drawing revision, critical features and required records before quotation. Inspection is agreed for the part and its application.
Part, quantity, application and requirements. You receive an inquiry reference straight away.
Send drawings or files to [email protected] and quote the reference.
We check manufacturability and reply with questions or a quotation.